
Quick answer
Do not paste ordinary milling feeds into a thread mill program. Start from approved tool and material data, convert cutting speed to spindle RPM, count effective circumferential cutting edges (not axial tooth count alone), apply the centre-path feed convention your CAM uses, then check engagement and machine limits before recording the first-part result. This page owns that conversion and unit check. It does not own the full programming verification checklist, and it does not own an interactive feed calculator.
CAM and process engineers often copy a face-mill or end-mill feed table into a thread mill cycle, then see broken teeth, oversized pitch, or a first article that fails the gauge. This Knowledge page owns how to start from approved cutting data, convert cutting speed to RPM, separate axial teeth from circumferential edges, check centre-path feed conventions, review engagement and machine limits, and record the first-part check before product inquiry. Start with the thread milling guide for cluster navigation, then use the thread mill selection guide when the candidate family is still open. Geometry contrasts between single-form and multi-form tools stay on the single-form vs multi-form thread mills guide. Callout reading stays on the metric and UN thread mill callouts guide. Hole and centre-path clearance stays on the thread mill diameter vs hole clearance guide. Aluminum mill-versus-tap tradeoffs stay on the sibling thread milling vs tapping aluminum guide. Product geometry and inquiry live on the thread mill product page.
Jump: Approved data · Vc to RPM · Effective edges · Centre-path feed · Engagement and limits · Record first part · Confirm · FAQ · Sources
Start from approved tool and material data
Write only inputs your plant has approved, or mark teaching fields clearly. Do not invent a "recommended" table on this page.
- Approved cutting speed (Vc or SFM): from the HC-approved traveler, proposal sheet, or controlled material card; leave blank if missing.
- Cutting diameter (D): the diameter used for speed conversion (usually cutting OD); keep it separate from minor diameter and entry choke owned on the clearance page.
- Material family and condition: as named on the drawing or traveler; do not upgrade the family to chase a remembered feed.
- Thread callout: system, nominal, pitch or TPI, form, and tolerance class already verified (leave blank fields blank).
- Coolant / through-tool note: plant method only; no invented pressure or life claim.
- Source stamp: document revision, approver, or Soft HOLD if the starting card is incomplete.
If any critical field is missing, mark it [NEEDS VERIFICATION] and Soft HOLD the programmed feed. Public threading literacy such as this threading knowledge overview and this thread milling process overview helps name helical generation without publishing an HENTRY feed table. Screw-thread handbook literacy such as this screw-thread handbook reference and units literacy such as this units and measurement guidance support naming systems and units honestly. Use the live thread milling programming guide for the machine-agnostic verification checklist; keep only feed-conversion fields on this traveler for now.
Start here: if Vc (or SFM) and D are not approved or labeled as teaching inputs, do not compute a production RPM.
Convert cutting speed to spindle speed
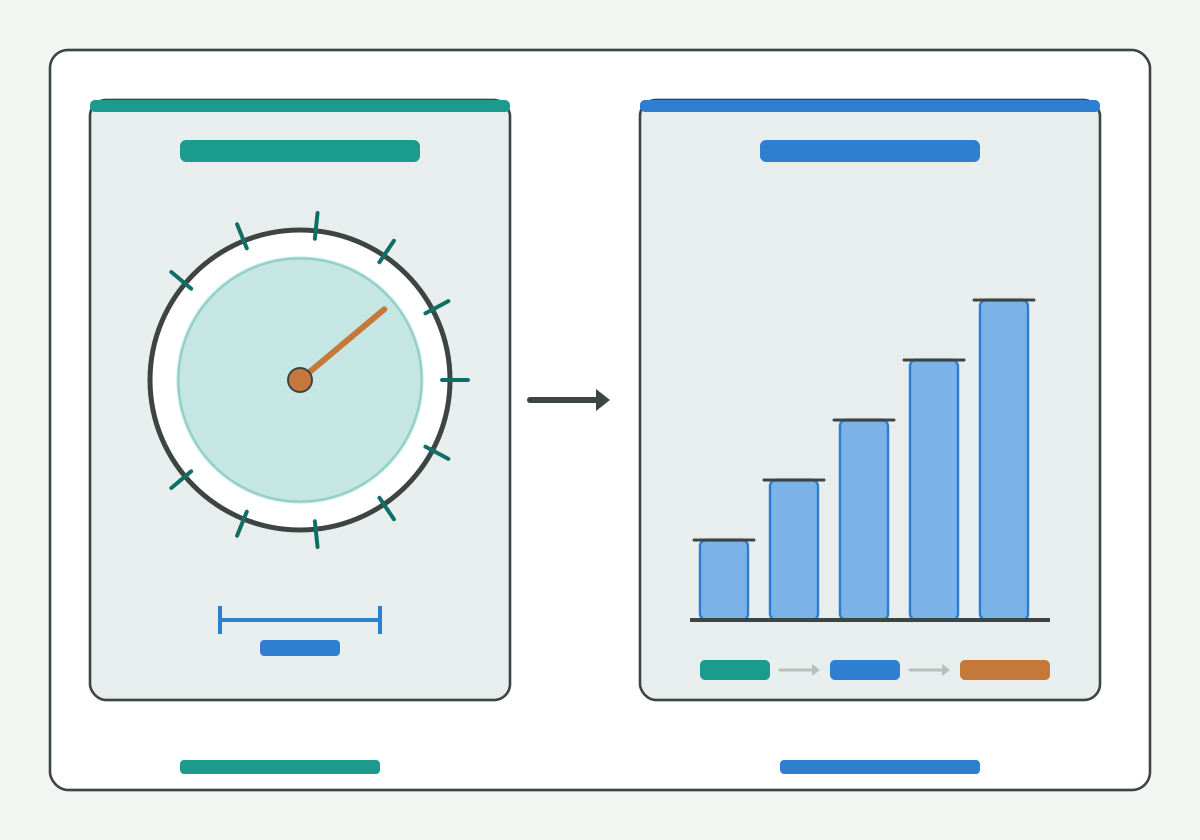
Illustration schematic: cutting speed to spindle RPM conversion panel with blank ticks - teaching layout only; not a catalog claim or ranked feed photo.
Convert approved cutting speed to spindle speed with the same unit system on both sides. Public machining literacy states the metric relationship as spindle speed n (rev/min) ≈ (1000 × Vc) / (π × D) when Vc is in m/min and D is in mm, and the inch relationship as n ≈ (12 × Vc_sfm) / (π × D_in) when surface speed is in ft/min and diameter is in inches. Write the formula source on the traveler; do not paste a remembered constant without naming units.
Unit check before you accept the number:
- Vc and D share a consistent unit pair (metric or inch), not a mixed pair;
- π is applied once; do not stack a second "rule of thumb" factor on top of an already converted RPM;
- controller display units (rev/min vs %) match what CAM posts;
- leave the RPM field blank rather than inventing a value when D or Vc is Soft HOLD.
Milling process literacy such as this milling process overview and machining data literacy such as this machining data literacy portal support naming Vc and n without migrating brand parameter sheets into this page. Metrology portals such as this public metrology laboratory entry and this international metrology portal keep units language tied to public sources.
Hypothetical teaching note (not a verified HC customer case; inputs labeled for unit check only): if a teaching card lists Vc = 80 m/min and D = 10 mm, the metric relationship above yields n ≈ 2546 rev/min before any plant derate. If someone instead pastes an unrelated end-mill RPM from another job, the failure is at the conversion gate, not at the gauge. Mark any production override [NEEDS VERIFICATION].
Use effective circumferential cutting edges
Thread mills carry axial teeth (form profiles stacked along the axis) and circumferential cutting edges that actually generate chips around the orbit. Feed-per-tooth math for programmed feed uses the effective circumferential edge count your CAM and tool definition agree on. Do not substitute axial tooth count alone when the control expects circumferential edges.
Write three separate fields when you have them:
- axial tooth / form count (geometry identity; see the single-form vs multi-form guide for family language);
- effective circumferential cutting edges z_eff used by the feed formula;
- source of z_eff (catalog note, CAM tool library, or measured confirmation).
If z_eff is blank or conflicted between the catalog sketch and the CAM library, Soft HOLD the feed and mark [NEEDS VERIFICATION]. Geometry contrast for single-form versus multi-form bodies stays on the single-form vs multi-form thread mills page; this page only consumes the edge count needed for feed conversion. Thread-milling product literacy such as this thread milling resource overview, this thread milling cutter overview, and this thread milling article overview helps name family language without migrating brand edge tables. Tool-family literacy such as this threading tools overview and this thread milling tools overview stays a neutral discovery aid. Geometry-inspection literacy such as this tool geometry inspection equipment overview helps name how shops confirm edge counts before the first article.
Hypothetical teaching note (not a verified HC customer case): a multi-form body may show several axial profiles while CAM still expects a smaller circumferential edge count for chip-load math. Pasting an ordinary end-mill "flute count" without checking z_eff is a conversion error, not a material problem.
Check centre-path feed conventions
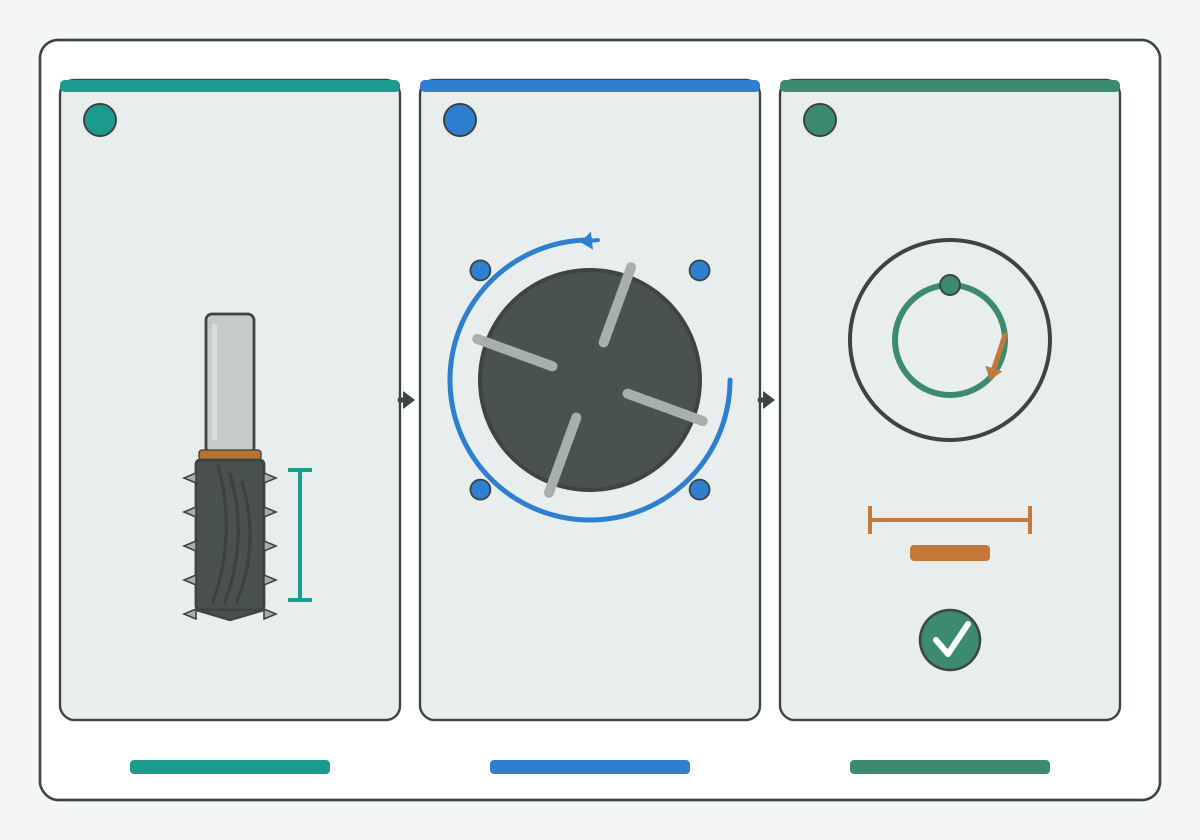
Illustration schematic: axial teeth versus circumferential edges plus centre-path feed check - unique gain for feed conversion; not a percentage rule, ranked catalog, or life claim.
Thread milling posts feed along a helical centre path. Many controls and CAM posts expect feed at the tool centre, while cutting-edge (peripheral) speed and chip load still depend on the orbit radius and engagement. Confirm which convention your post uses before you accept a feed number:
- centre-path feed (tool centre follows the programmed helix);
- peripheral / cutting-edge referenced feed (if your post converts explicitly);
- units: mm/min or inch/min at the path the control actually interpolates.
Do not paste an ordinary pocket-milling feed verbatim into the thread mill cycle. Recompute from approved chip-load intent × z_eff × spindle speed under the centre-path convention your plant documents. Hole and orbit clearance context stays on the thread mill diameter vs hole clearance guide; this page stops at feed convention and unit check. Soft note (guide forthcoming, no empty hard link): an interactive feed calculator page will reuse these input definitions when published; until then, keep symbols, D, and z_eff on this traveler and do not hang an empty hard link.
Toolholding literacy such as this tool-holder interface overview and this toolholding tips overview helps name runout and projection checks that still change effective engagement at the centre path. Coolant path literacy such as this coolant concentration measurement method supports fluid-control language when chips pack in a tight orbit, without inventing an HENTRY pressure guarantee. Standards literacy such as this codes and standards portal, this national standards overview, and this international standards catalogue entry support naming systems without publishing an HENTRY feed matrix.
Hypothetical teaching note (not a verified HC customer case): if a teaching card lists an approved chip-load intent of 0.02 mm/edge, z_eff = 4, and n ≈ 2546 rev/min, a centre-path feed estimate is chip-load × z_eff × n before any plant derate (about 204 mm/min in that teaching arithmetic). If the post expects centre-path feed and the programmer pastes a peripheral pocket feed from another job, the first failure mode is usually oversize engagement or broken teeth, not a "wrong material." Label teaching arithmetic clearly; do not treat it as a customer recommended table.
Review engagement and machine limits
After the conversion math is written, review engagement and machine limits as a separate gate:
- radial and axial engagement for the planned pass (full profile versus multiple passes);
- spindle speed ceiling and torque / power available at that RPM;
- feed ceiling of the interpolating axes at the programmed centre-path radius;
- holder projection and stick-out that raise bending risk at the same feed;
- coolant delivery adequate for the orbit (method only; no invented life %).
If engagement or machine limits are unknown, Soft HOLD and mark [NEEDS VERIFICATION]. Soft note (guide forthcoming, no empty hard link): pass strategy, spring passes, and finish-pass detail will sit on a dedicated pass-strategy Knowledge page when published; stainless and chatter-focused essays will sit on a dedicated stainless Knowledge page when published. Keep only the limit check that blocks the converted feed on this traveler. Machining research literacy such as this peer-reviewed machining research journal overview and this machining process and tool development research overview keep method language tied to public sources. Tapping literacy such as this tapping knowledge overview and threading article literacy such as this threading article overview are contrast only: a tap feed story does not replace thread-mill centre-path conversion. Substrate blank literacy such as this carbide rod blank portfolio overview and regrind literacy such as this regrind inspection and economic review overview support tool-body talk without life percentages.
| Field | What you write | If missing |
|---|---|---|
| Approved Vc / SFM | From HC card or labeled teaching input | Soft HOLD; do not invent |
| Cutting diameter D | Diameter used in RPM conversion | Stop; do not guess from nickname |
| Spindle n | Converted RPM with unit pair named | Mark [NEEDS VERIFICATION] |
| z_eff | Effective circumferential edges | Do not substitute axial tooth count alone |
| Feed convention | Centre-path vs peripheral (plant post) | Do not paste ordinary milling feed |
| Programmed feed | Value under the named convention | Leave blank rather than invent |
| Engagement / machine limits | Pass plan, RPM/feed ceilings, stick-out | Soft note: pass-strategy guide forthcoming |
| First-part status | Pass / fail / hold | Do not release the traveler |
Record and inspect the first part
Close the page task only after the traveler records a first-part result next to the print revision:
- approved Vc / D / n / z_eff / feed convention / programmed feed as posted;
- pass / fail / hold for gauge or optical check of the thread;
- any Soft HOLD fields still open (compensation detail, controller-specific screens, pass strategy);
- stop conditions: broken tooth, oversize / undersize pitch evidence, abnormal noise / load that forces a hold;
- material family and blank condition as cut;
- acceptance method and who signed the first-part row.
Procurement checklist fields may stay blank; blank is better than invented digits. Hard-link live: blind-hole thread milling depth. Soft note (guides forthcoming, no empty hard links): cutter compensation essays, Fusion or Haas controller setup screens, and internal/external direction essays will sit on dedicated Knowledge pages when published. When the feed conversion and first-part row pass on paper, move to product review instead of another remembered feed paste.
How HENTRY supports the feed conversion
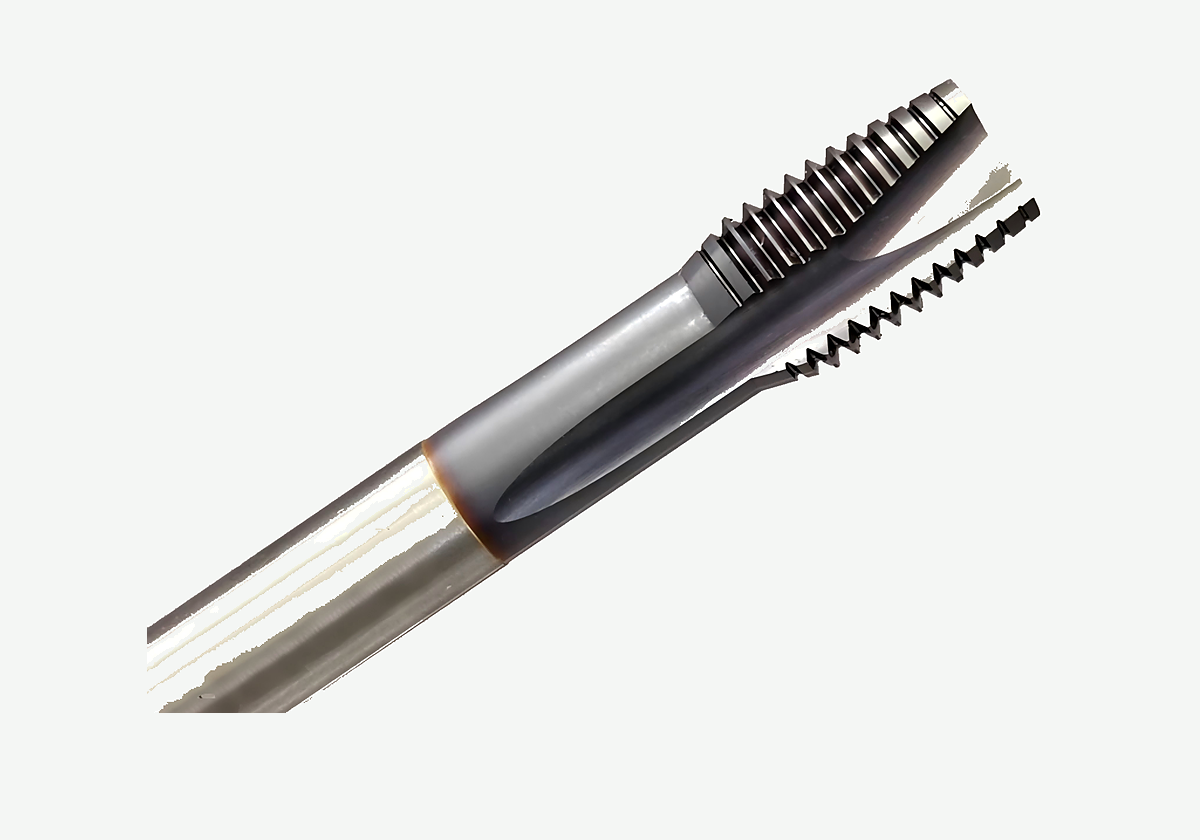
Product rematte of tip, flutes, and shank on a thread-mill body - not a ranked catalog, feed table, or life claim.
HENTRY manufactures drawing-based cutting tools, including solid carbide thread mills. When approved cutting data, RPM conversion, effective circumferential edges, and centre-path feed convention are written - even with blank Soft HOLD fields - you can move from this Knowledge slice to a product review instead of another ordinary milling feed paste. Public threading-resource literacy such as this threading resources hub remains a discovery aid only; do not migrate brand parameters into an HENTRY proposal.
Next action: Review the matched tool and validation inputs. When the controlled drawing and traveler fields are ready to send, open the custom cutting tool RFQ. Quotation turnaround after complete drawings is typically 1-2 working days for engineering review, not a promise of unvalidated cutting data.
Thread mill speeds and feeds FAQ
Can I paste ordinary milling feeds into a thread mill program?
No. Recompute from approved cutting speed to RPM, apply effective circumferential cutting edges, and use the centre-path feed convention your CAM posts. Ordinary pocket or face-mill feeds skip those gates and are a common first-article failure mode.
How do axial teeth differ from circumferential cutting edges for feed math?
Axial teeth describe form profiles stacked along the tool axis. Circumferential cutting edges are the edges that generate chips around the orbit and that feed-per-tooth math usually needs. Do not substitute axial tooth count alone when the control expects circumferential edges.
What does centre-path feed mean?
Centre-path feed is the feed rate referenced to the tool centre as it follows the helical orbit. Confirm whether your post expects centre-path or a peripheral conversion before you accept the programmed number, and keep units consistent.
Can I program feeds without approved starting data?
No for production. If Vc, diameter, or edge count is missing, mark the field for verification and Soft HOLD. Teaching arithmetic must be labeled hypothetical and must not be treated as a customer recommended table.
How does this page relate to a feed calculator page?
This page locks input definitions, unit checks, and conversion order. An interactive calculator, when published, should reuse those definitions rather than invent new symbols. Until that page is live, keep the traveler fields here and do not rely on an empty link.
Sources and related guides
Authoritative literacy (neutral anchors; discovery only; not HENTRY catalog limits or life claims). Link check Asia/Shanghai 2026-10-31:
- threading knowledge overview
- thread milling process overview
- milling process overview
- tapping knowledge overview
- thread milling resource overview
- thread milling cutter overview
- threading resources hub
- thread milling article overview
- threading article overview
- threading tools overview
- thread milling tools overview
- tool-holder interface overview
- toolholding tips overview
- coolant concentration measurement method
- tool geometry inspection equipment overview
- screw-thread handbook reference
- units and measurement guidance
- codes and standards portal
- national standards overview
- international standards catalogue entry
- public metrology laboratory entry
- international metrology portal
- peer-reviewed machining research journal overview
- machining process and tool development research overview
- machining data literacy portal
- regrind inspection and economic review overview
- carbide rod blank portfolio overview
Related live pages: thread milling guide · thread mill selection guide · single-form vs multi-form thread mills · metric and UN thread mill callouts · thread mill diameter vs hole clearance · thread milling vs tapping aluminum · thread mill product page. Also see the live thread milling programming guide and blind-hole thread milling depth. Soft note only (no empty hard links): feed calculator, pass strategy, stainless / chatter, controller setup, compensation, and direction Knowledge pages are forthcoming.
When the feed conversion and traveler fields are ready, Review the matched tool and validation inputs.