
Product Detail
Carbide Reamers for Precision Holes
Provide your finished-hole requirements and pre-hole conditions to review carbide reamer geometry, dimensions, and validation needs.
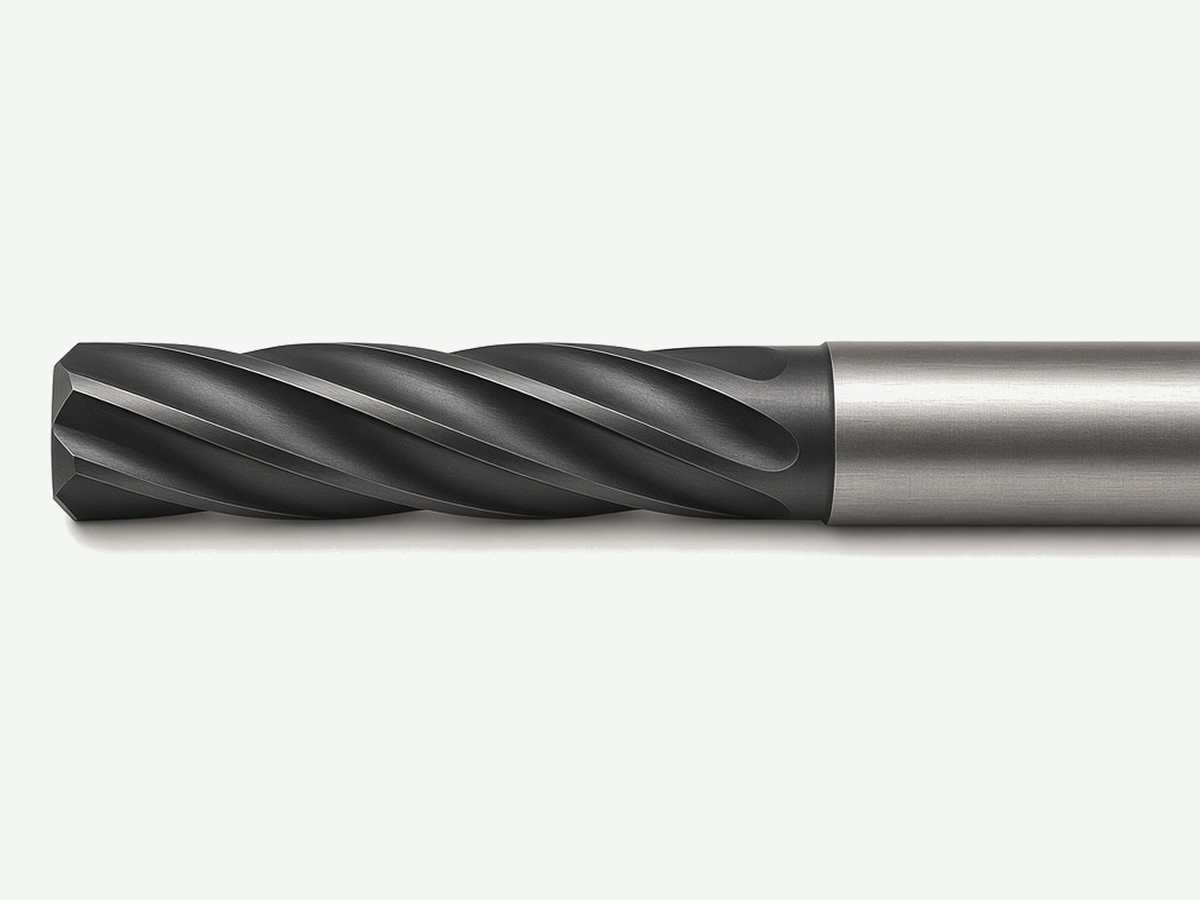
Carbide reamers · precision holes
Carbide Reamers for Precision Holes
Provide your finished-hole requirements and pre-hole conditions to review carbide reamer geometry, dimensions, and validation needs.
- Carbide family under the reamer hub — PCD reamers stay on their own page
- Tool make size is not the same as guaranteed hole tolerance
- Pre-hole quality still limits what reaming can correct
Solid carbide and carbide-tipped construction
Keyword lists may include both solid and tipped constructions. Purchase paths appear only when supply is confirmed. If only one construction is available, the other card is hidden at publish time.
Solid carbide reamer
Monolithic carbide body and cutting portion. Suited to rigid setups and materials where carbide geometry is appropriate. Dimensions confirmed to your drawing.
Request solid carbide reviewCarbide-tipped reamer
Carbide cutting edges on a supporting body. Availability and body design vary — do not treat keyword presence as stock proof.
Request tipped construction review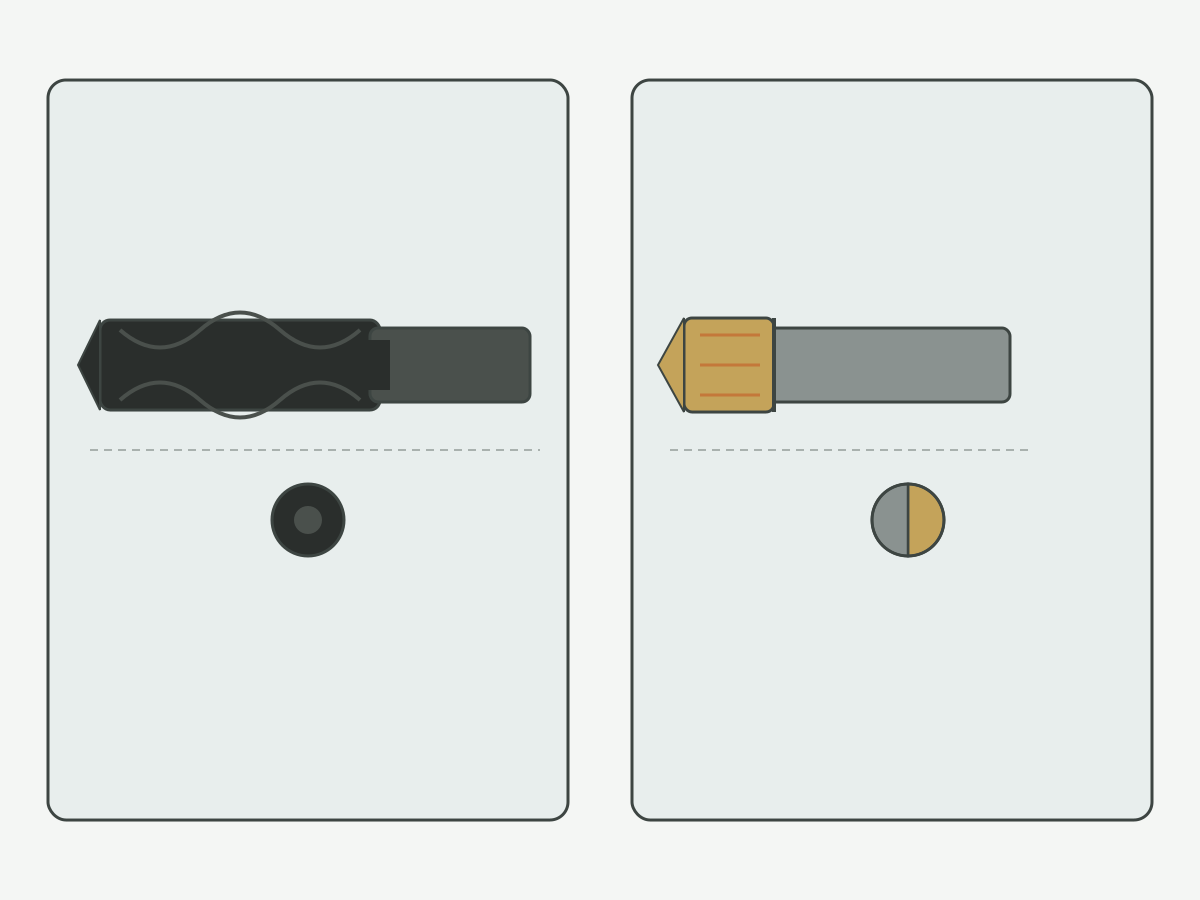
Diameter and tolerance needs
State the finished hole target (size, roundness, cylindricity, surface). Tool manufacturing size is set from that target and process allowance. Result claims need application evidence — not generic accuracy slogans.
| Customer states | Engineering uses it for | Not claimed here |
|---|---|---|
| Finished hole size / class | Reamer make diameter | Guaranteed hole class without process data |
| Roundness / cylindricity | Geometry & setup review | Correction of all prior-op error |
| Surface finish target | Edge prep / feed discussion | Life or % improvement figures |
Workpiece material and pre-hole
Reaming finishes an existing hole. Send pre-hole size, allowance consistency, alignment condition, and material. A reamer is not a universal fix for drilling error.
- Pre-hole diameter and method (drill, bore, etc.)
- Stock allowance and its variation across the lot
- Axis alignment / runout context
- Workpiece material and hardness band if known
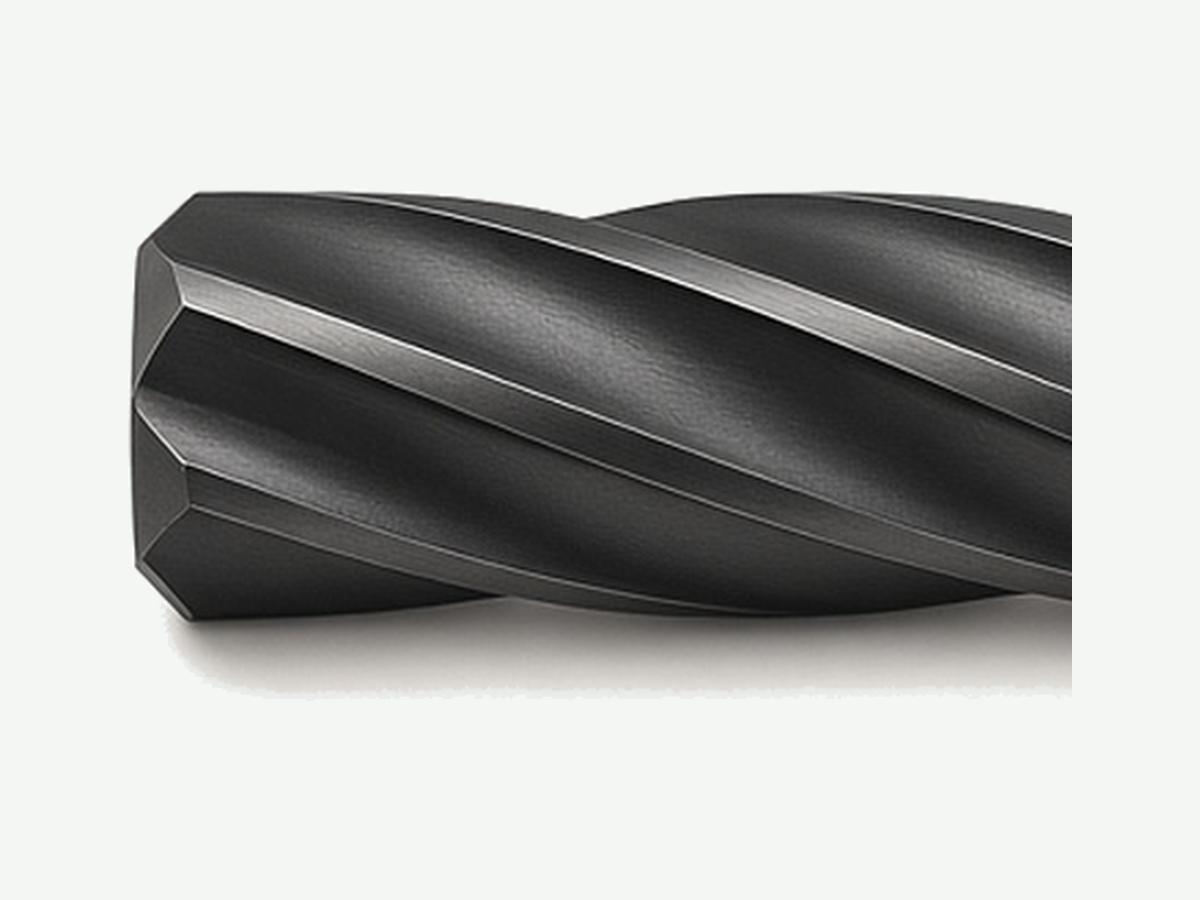
Coolant, flute, and length options
Call out cutting diameter, flute length, overall length, shank diameter, and usable reach with units. Through-coolant and flute count appear only when verified for the quoted design.
Unlisted options = engineering review, not “full series in stock.”
Sample validation and RFQ
Agree measurement method, gage, and lot before discussing production supply. Inspection excerpts appear only with permission and version control.
Quotation typically takes 1–2 working days after complete drawing information (quotation only).
Selection guide
| Model / series | Solid / tipped | Ø mm | Flute L mm | OAL mm | Shank Ø mm | Flutes | Coolant | Supply |
|---|---|---|---|---|---|---|---|---|
| 按图纸 | Confirm | 按图纸 | 按图纸 | 按图纸 | 按图纸 | Review | Review | Engineering RFQ |
Catalog rows added only after product approval. Related: reamer tool overview · PCD reamer.
Carbide reamer FAQ
How do solid and tipped carbide reamers differ?
Solid reamers are monolithic carbide. Tipped designs put carbide cutting edges on a supporting body. Availability depends on confirmed supply — keywords alone do not prove both are stocked.
What pre-hole information should I send?
Pre-hole size and method, allowance, alignment notes, material, and the finished-hole target. Incomplete pre-hole data delays a firm geometry recommendation.
How are custom tolerances confirmed?
From your finished-hole requirement and process evidence. Tool make size is engineered to the print; hole results still depend on setup, pre-hole, and measurement method.
When should I look at PCD instead?
For repeat non-ferrous / aluminum finishing where PCD is the better wear path. Use the PCD reamer page — this page stays on carbide.
Request a Reamer Review
Page N005 · Product Carbide Reamers for Precision Holes.
Guangdong Hentry Tool Technology Co., Ltd · Brand: HENTRY