
Die and Mold Tooling for Hardened Steel: End Mills, Drills and Reamers
The insert came back from heat treatment, the finish pass is half done, and the ball nose has already chipped at the tip — or the long-reach tool is singing in the bottom of a deep rib and the wall is coming out tapered. What helps is knowing which part of the tool is failing, what to change, and who can grind a version that fits your cavity.
Below: the failure you see, the design lever that answers it, the HENTRY end mill page that covers each shape in depth, how the drilled and reamed holes in the same plates are handled, and the information we need to quote a custom tool from your drawing.
Why end mills fail in hardened mold and die steel
Mold and die steels are often machined after heat treatment, so the cutter meets a hard, abrasive workpiece on every pass. The edge has to stay sharp enough to cut and tough enough not to break, and the cavity shape usually forces long reach, small radii and changing engagement at the same time. Name the failure before choosing a tool.
Edge chipping on entry and at the corners
In a hard or interrupted cut, a sharp tool corner carries the impact on almost no edge length, so that is usually where chipping starts. Chipping that starts right after entry, or only on one flute, can also come from runout or a weak setup.
Flank wear before the cavity is finished
In hot, hard contact the edge wears and loses its shape. On a finish pass that matters twice: the tool cuts undersize as it wears, and changing tools part-way through a finish pass can leave a visible line where the two passes meet.
Deflection and chatter on long reach
Every extra length of neck or stick-out makes the tool easier to bend. Deflection shows up as a wall that tapers toward the bottom, a form that cuts undersize at depth, or chatter marks on deep ribs.
Cusps, rubbing and poor surface finish
A ball nose leaves a scallop between passes, and near its center the cutting speed drops to zero, so on flat areas it rubs instead of cutting. Runout and a worn tip show up in the finish too.
Deep cavities, draft walls and tight internal corners
Some features cannot be reached with a straight, full-length tool at all: a pocket below a tall wall, a drafted side wall that a straight tool can only step down, or a back-side edge hidden from a vertical spindle.
How the tool design answers each problem
| What you see | Design lever | What we need from you |
|---|---|---|
| Edge chipping | Carbide grade tough enough for the cut; edge preparation; corner radius instead of a sharp corner where the drawing allows | Measured hardness, entry conditions, photos of the chipped tool |
| Flank wear mid-cavity | Grade and coating matched to your steel and coolant mode | Steel grade, hardness, wet / dry / MQL |
| Deflection and chatter | Shortest neck that clears the part; flute length only where it cuts; flute count, helix or unequal pitch to break up chatter | Cavity depth, wall height above the feature, holder and stick-out |
| Cusps and rubbing | Ball or corner radius sized to the model; tool tilted away from the ball center on a five-axis machine | Smallest concave radius, finish target, three- or five-axis machine |
| No access | Long-neck, tapered or lollipop form ground to the drawing | Drawing or 3D model with the feature and its tolerances |
Carbide grade and edge preparation
Hardness pushes the grade choice in two directions: the edge must resist wear, yet stay tough enough not to break when engagement changes around a cavity. Edge preparation decides whether the cutting edge, and the coating on it, has a stable base; an unprepared sharp edge that chips loses its coating with it. We set the grade from your steel, the measured hardness and the stage, and confirm grain size and binder content at drawing review.
Geometry: end shape, flute count, helix and pitch
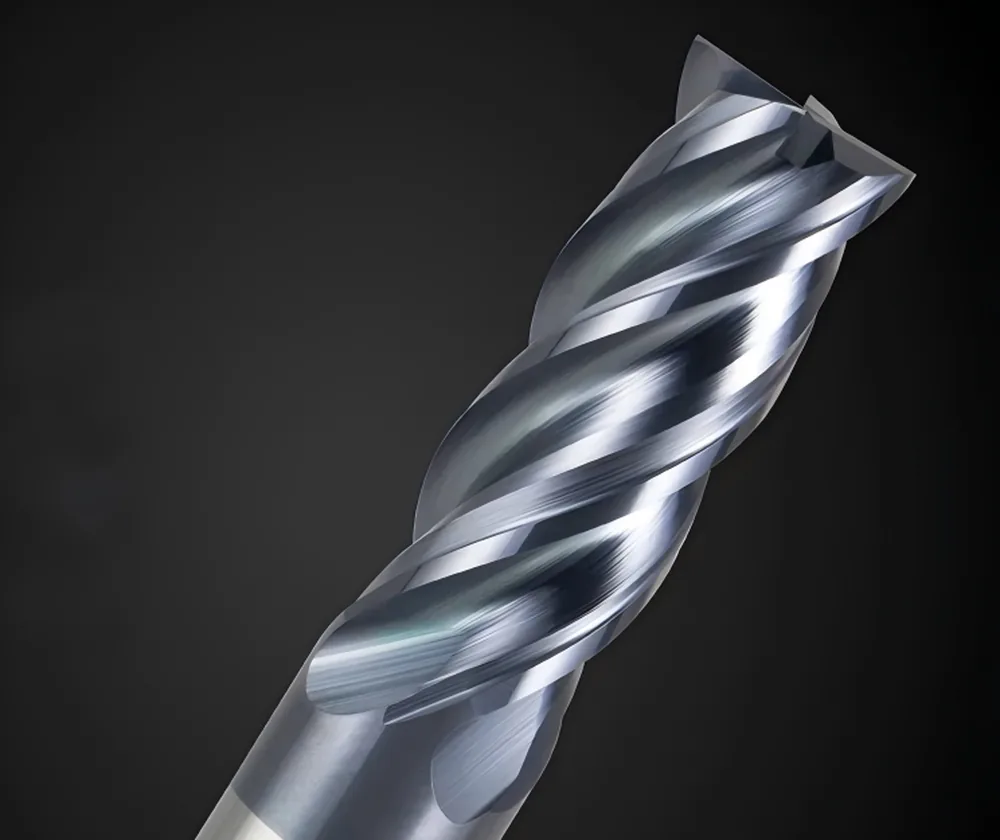
End shape follows the feature: ball nose for freeform surfaces and full fillets, corner radius for flat floors with a drawn fillet, square only where a sharp floor corner is required. More flutes suit finishing in steel, fewer suit slots that need chip room, and unequal pitch or helix helps where chatter is the problem.
Coating chosen for your steel and process
There is no fixed coating list for die and mold end mills. The coating is chosen for the tool and the workpiece, for example an AlTiN-type coating where heat builds up at the edge in hot, dry or MQL cuts in steel. After a regrind the fresh edge is bare carbide; whether we re-coat follows your requirement. CVD coatings are available on request through a partner.
Neck relief and reach
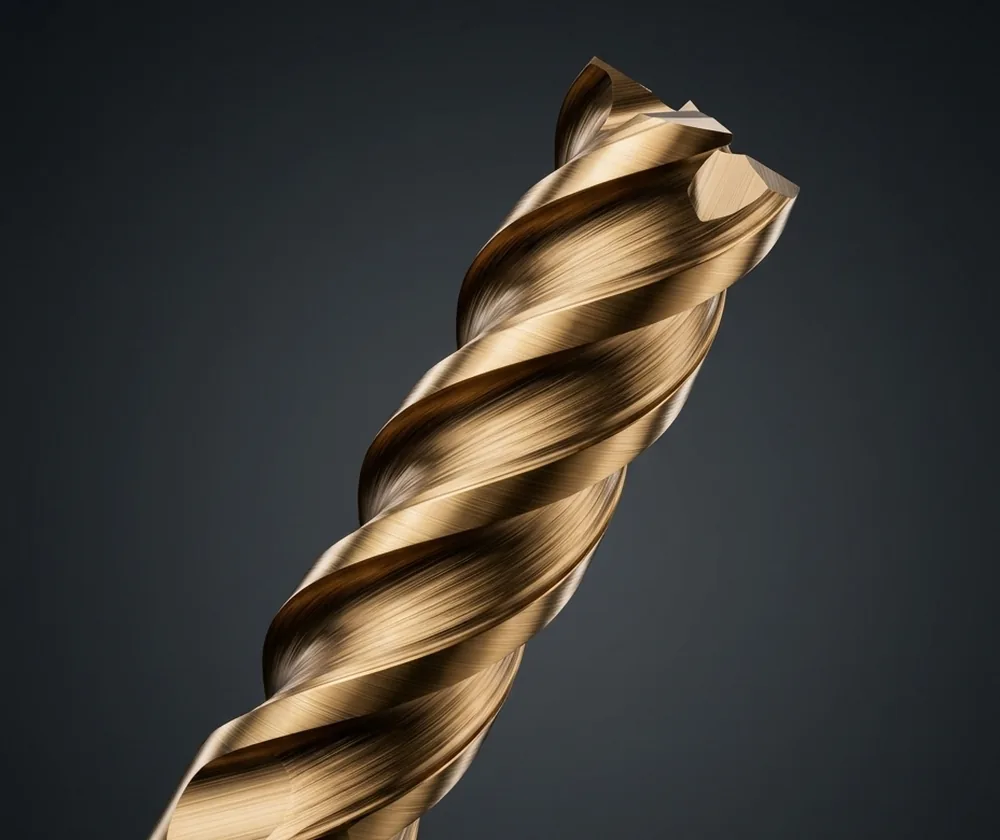
Deep mold features need reach, and reach costs stiffness. A relieved neck lets the cutting end work below a tall wall without the shank rubbing, but each extra length lets the tip bend further away from the path. So we size the neck to the deepest point the tool must reach and no longer. That is why the RFQ asks for the wall height above the feature as well as the feature itself.
Special forms for molds and dies
Five solid carbide special forms are ground to customer drawings and quoted only after the form, reach and holder have been reviewed:
- Tapered: for draft walls on molds and dies and for tapered slots; the side angle is ground into the tool instead of being built up from many small CAM steps.
- Long-neck: short cutting length, relieved neck: the answer when the deep rib or pocket floor sits below a tall wall.
- Lollipop: a ball-shaped head on a slim neck reaches back-side edges and hidden faces that a straight tool cannot touch, typically on five-axis machines.
- Dovetail: for the angled sides of slideways, guides and dovetail locating features.
- T-slot: for T-shaped slots in steel and cast-iron machine tables and fixture plates.
Which end mill for which die and mold stage
Split the job by stage; one tool rarely roughs and finishes a hardened cavity well. Each standard shape has its own HENTRY page with sizing detail, linked in the table below.
Keep PCD for aluminum and other non-ferrous mold work: in steel the hot tip lets iron react with the diamond, so steel molds are cut with carbide.
Holes in the same plates are listed at the end of the table and covered in the holemaking section below.
| Stage / feature | Usual tool | Where the detail is |
|---|---|---|
| Bulk stock removal in ferrous blocks | Serrated / chipbreaker roughing end mill | Roughing end mill |
| Shallow floors and pocket decks at high feed | Solid high-feed end mill, light axial depth | High-feed end mill |
| Semi-finishing where sharp corners chip; floors with a drawn fillet | Corner radius (bull nose) end mill | Corner radius end mill |
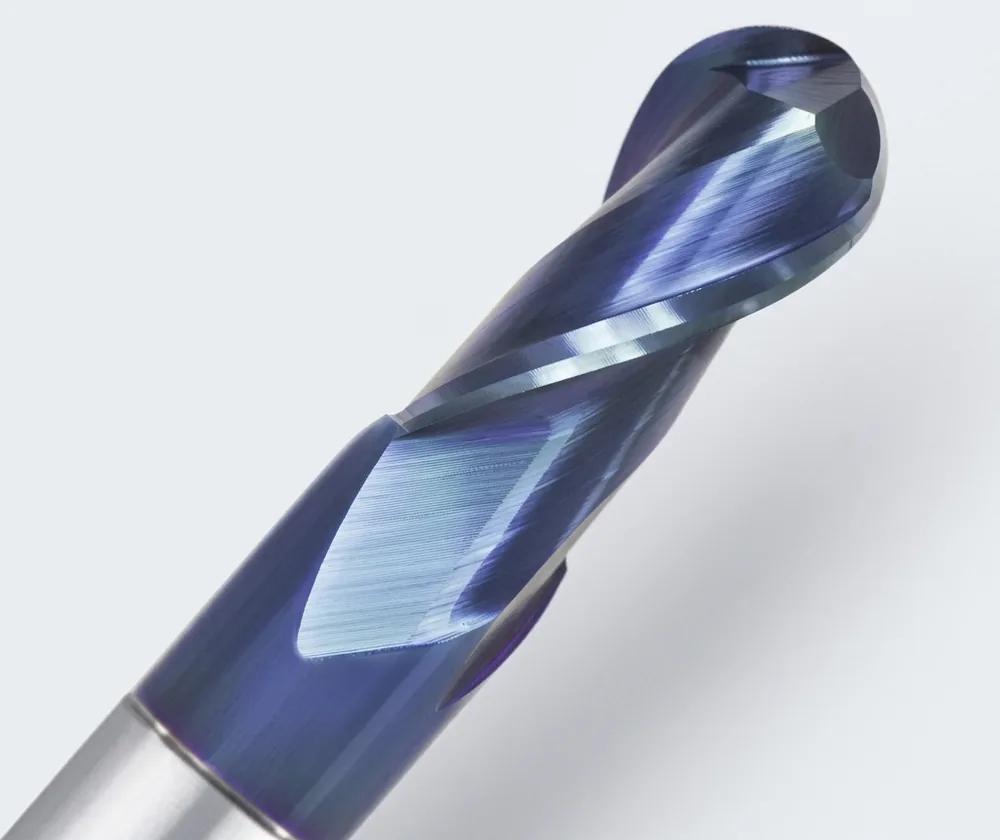
| 3D finishing of surfaces and concave fillets | Ball nose end mill sized to the smallest model radius | Ball nose end mill |
| Flat floors with a sharp floor corner | Square end mill | Square end mill |
| Deep, drafted or hidden features | Long-neck, tapered or lollipop special form | Custom end mill manufacturer |
| Aluminum mold inserts and parts | PCD ball nose (not for steel molds) | PCD ball nose end mill |
| Cooling-channel, ejector-pin and bolt holes in hardened or pre-hardened plate | Solid carbide drill built from the measured hardness; deep-hole or through-coolant design for long channels | Drills for hardened steel · Solid carbide drills |
| Dowel and guide-pin bores in hardened or pre-hardened steel | Drill, then solid carbide reamer where the hardness allows | Solid carbide reamer, quoted from your drawing |
| Bores in aluminum mold or fixture parts, non-ferrous or composite components | PCD reamer | PCD reamer |
Drilling and reaming holes in die and mold plates
A mold base or die set is not only cavities. The same plates carry cooling channels, ejector-pin holes, dowel and guide-pin bores and bolt holes, and many of them are drilled in plate that is already hardened or pre-hardened. These are HENTRY's core tool lines, built to your drawing like the end mills above. For the route across the whole part, from what to cut before heat treatment to what to finish after it, see our guide to machining hardened steel.
Drilling hardened and pre-hardened mold plate
Pre-hardened plate goes onto the machine as it arrives, so the drill is designed from the hardness at the spot it will cut and from how the plate was hardened. Hardness can change through a thick plate, which is why we ask for the mill certificate and your own reading. A scaled, ground or EDM-affected entry surface, or a sloping entry face, hits the drill corner before the point has centered; in that case a spot or center operation often goes first. Our solid carbide drills for hardened steel are designed around exactly these inputs, and the wider solid carbide drill range covers custom diameters, lengths, step and chamfer features and through-coolant layouts.
Cooling channels and ejector-pin holes
Cooling channels are long holes, and on long holes depth breaks more drills than hardness does: chips have to travel the full length and heat builds at the point. Long channels usually call for a deep-hole carbide drill or a through-coolant drill, matched to whether your machine has through-spindle coolant. Ejector-pin holes have to stay straight and on size so the pin slides freely, which is why their tolerance and depth belong on the RFQ.
Dowel and guide-pin bores: solid carbide reamers
Where a dowel or guide-pin bore needs a finished size or surface that drilling alone does not give, the hole is drilled and then reamed. In hardened or pre-hardened mold steel that finishing step is a solid carbide reamer, where the hardness allows; the reamer, its stock allowance and the pre-hole are confirmed together at drawing review.
Where PCD reamers fit and where they do not
PCD reamers are for aluminum mold and fixture parts, copper and brass components, and composite parts, where repeat production makes a wear-resistant diamond edge worthwhile. They are not for hardened steel or any other ferrous bore: diamond reacts with iron at cutting temperature. On a steel die set, the drill and the reamer are carbide. See PCD reamers for the non-ferrous side.
Custom die and mold end mill options
We do not work from a stock size list. Tell us which dimensions the part fixes and which are open; we propose the rest and send a tool drawing for approval.
Standard range
No stock size list; each tool is ground to your drawing.
Customizable
Cutting diameter · flute length against reach · neck relief · flute count, helix, unequal pitch · ball radius, corner radius or chamfer · shank and overall length to suit your holder · coating · tapered, long-neck, lollipop, dovetail or T-slot form · laser marking of your brand or part number.
Confirmed at drawing review
Form tolerance that can be held at your reach · carbide grade · coating type · sample quantity and lead time.
What a new cutter will not fix
- Runout, long stick-out or packed chips. When these cause the chipping, a tougher cutter just fails later; fix the holder, stick-out or toolpath first.
- A truly sharp vertical corner. A rotating tool always leaves its own radius where two walls meet; that corner needs another process.
- PCD on steel cavities. For hardened steel the answer is carbide.
- Hardness we have to guess. Without the measured hardness and where it was taken, any grade and coating choice is a guess.
From drawing to repeat batches
- Feasibility first: your cavity drawing, hardness, holder and machine are reviewed together, and anything that cannot be held at the requested reach is raised before a quote.
- Approved tool drawing: grinding starts only after you sign off the tool's dimensions.
- Measured against your drawing: each tool's form and sizes are checked against that approved drawing; inspection results can ship with the tools on request.
- Trial on your machine: when the first tools must prove themselves before a batch, our sample validation process agrees the acceptance criteria in writing first.
- Repeat, regrind, re-coat: repeats are ground to the same approved revision; worn tools can be reground at HENTRY, with re-coating if you ask for it.
Only have the worn tool? It can be the starting point; see replacing a special cutting tool from a sample. Distributors and own-brand lines can have their brand or part number laser-marked on the tool; labels and packaging follow our private-label cutting tools terms.
Die and mold end mill RFQ: what to send
Send what you have; gaps are filled at drawing review.
- Steel grade, heat-treat state and measured hardness, with where it was taken
- Drawing or 3D model of the cavity, with the smallest concave radius, draft angles and fillet callouts
- Cavity depth and the wall height above the feature
- Stage: roughing, semi-finishing or finishing, and the finish target
- The current tool and how it fails (chipping, flank wear, chatter, poor finish or breakage), with photos
- Machine (three- or five-axis), holder, stick-out, coolant (wet, dry or MQL)
- Holes: diameter, depth, tolerance, blind or through, and whether they are drilled before or after hardening
- Quantity, expected repeats, regrind plan, and any marking under your brand
Die and mold end mill FAQ
What end mill should I use for hardened mold steel?
Start from the feature and the stage, then the hardness. A ball nose finishes freeform surfaces, a corner radius tool handles floors and semi-finishing where sharp corners chip, and the carbide grade and coating are chosen for the measured hardness and coolant mode.
Can one end mill rough and finish a hardened cavity?
Rarely well. Roughing removes stock under heavy load, while finishing needs a sharp, round edge for the final surface. Splitting the stages protects the finishing tool and the cavity.
Why does my end mill chip in hardened steel even with a hard-milling coating?
A coating only protects an edge that is stable underneath it. Chipping usually comes from a grade or edge preparation that is too weak for the cut, a sharp corner taking impact, or runout and long stick-out in the setup.
Which special end mill forms help with deep cavities and draft walls?
Long-neck tools reach features below a tall wall, tapered tools cut draft walls with the angle ground into the tool, and lollipop tools reach back-side edges. Each is ground to your drawing after a reach and form review.
Which reamer fits dowel and guide-pin bores in a mold?
In hardened or pre-hardened mold steel, a solid carbide reamer after drilling, where the hardness allows, confirmed at drawing review. PCD reamers are for aluminum mold and fixture parts and other non-ferrous or composite components, not for steel, because iron wears a diamond edge quickly as it heats up.
Do you regrind, re-coat and mark die and mold end mills for distributors?
Yes. Worn custom end mills can be reground at HENTRY, re-coating follows your requirement, and we can laser-mark your brand or part number on the tool.
Send the drawing and the measured hardness
Share the cavity or plate drawing, the steel with its measured hardness, the holes to drill or ream, and what the current tool is doing wrong. Our engineers reply with what can be held, what needs a change of process, and a tool drawing for you to approve.