
Hydraulic Spool Bore Finishing — Allowance, Ream, RFQ
The spool bore gauged on diameter and still stuck the valve—or first-off went oval after unclamp because the reamer chased a crooked pre-hole and an unknown stock band.
This page owns hydraulic spool bore finishing: what “finished” means on the spool feature, pre-hole and allowance discipline, PCD ream path when the print demands it, and the RFQ pack. Full valve-body hole-pattern mapping stays on Hydraulic Valve Body Machining. Intersecting manifold drilling stays on Hydraulic Manifold Drilling. XRZ quotes from your valve-body print, material, measured runout, and machine constraints—not from a catalog “valve reamer” label (sample validation · Custom Cutting Tool RFQ).
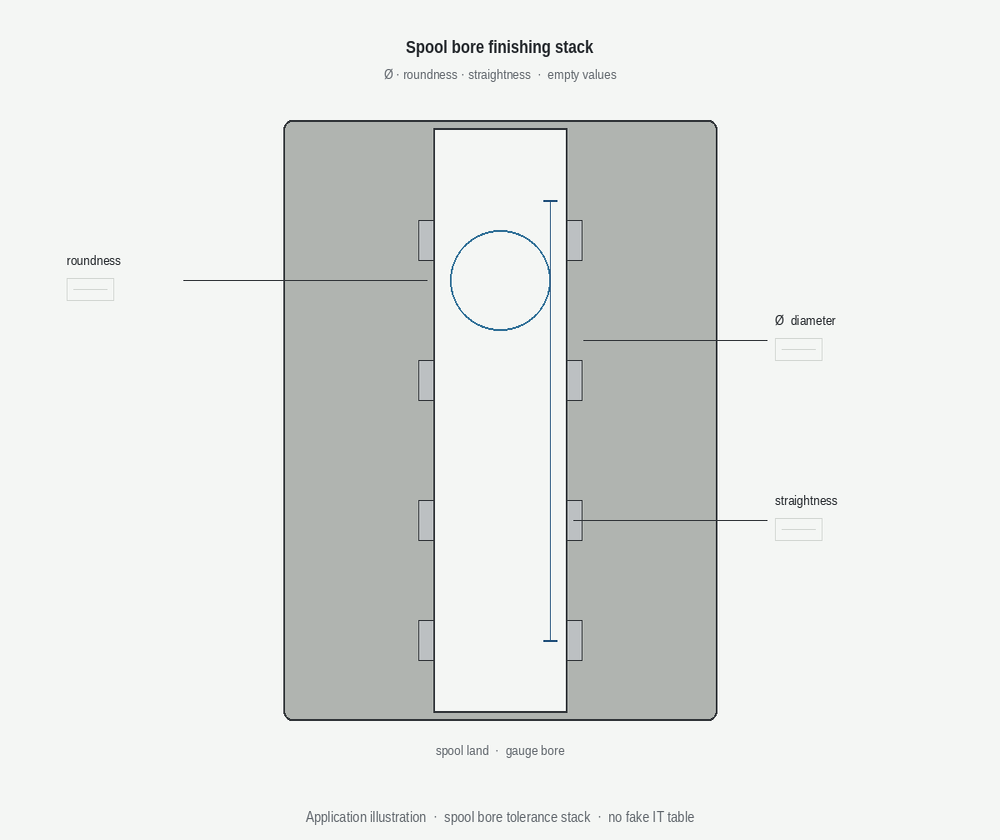
What “finished” means on a spool bore
| Callout (heuristic — not a fake IT promise table) | Why it drives tooling |
|---|---|
| Diameter (Ø) + tolerance band | Freezes ream vs create-hole scope |
| Roundness / oval after unclamp | Clamp + thin-wall reality before finish geometry |
| Straightness / alignment along land | Guidance posture and setup plan |
| Finish / chatter marks | Runout, stickout, edge prep — soft diagnosis only |
Do not treat every land on the valve body as a spool finish bore. Clearance and non-gauge openings stay on the create-hole path when the gauge allows. Soft diagnosis: PCD reamer pre-hole quality · PCD reamer chatter diagnosis.
Pre-hole & allowance (soft Knowledge — do not restate)
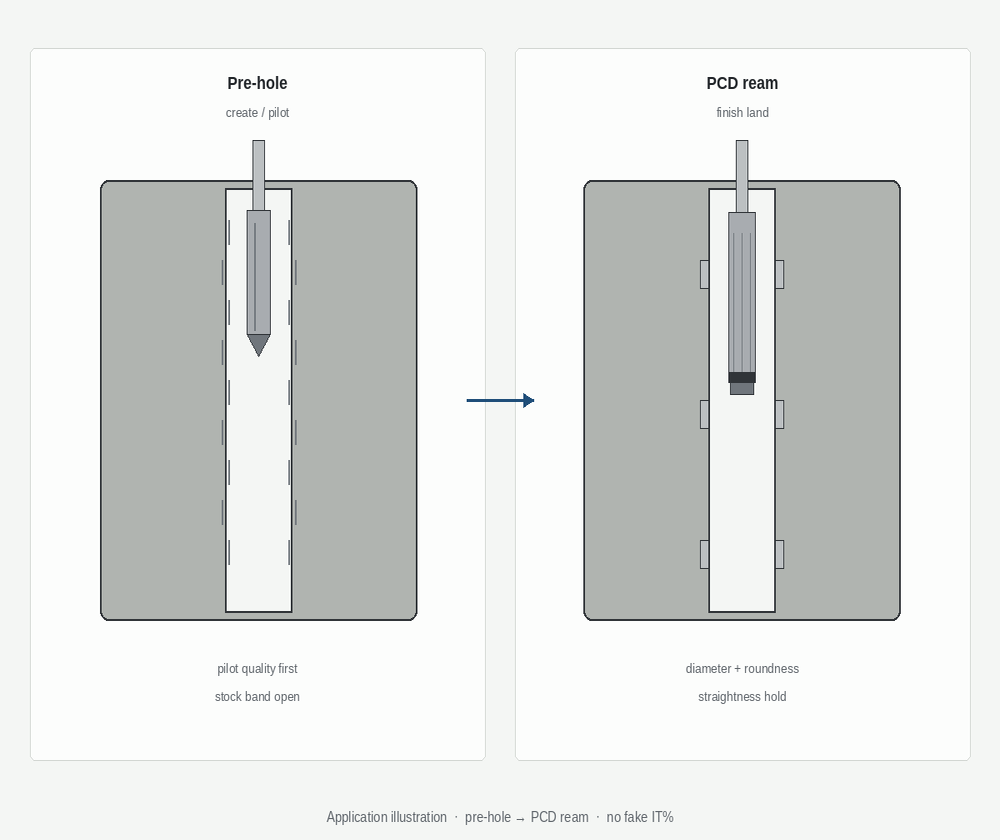
A stable spool finish usually starts with an honest pre-hole and a measured allowance band before freezing reamer geometry. Do not invent a universal stock number on this page.
Soft Knowledge (do not paste H2s): PCD reamer allowance & pre-hole size · Blind / through / cross reaming. Fine boring may appear at the process boundary on some spool lines—XRZ does not claim a full fine-boring pillar here; mark that requirement on the RFQ if your route needs it.
PCD ream path + when step/form is enough
- Create-hole with a carbide drill matched to material and coolant — Solid Carbide Drill.
- Measure the incoming diameter band before freezing reamer allowance.
- Finish with a Custom PCD Reamer when diameter, roundness, or finish must hold on the spool land.
Step/form PCD earns a station when the spool print carries multi-diameter lands or shoulders that collapse into one guided pass—not as a default slogan. Soft decision: Drill-then-ream vs PCD combination · product Combination Drill-Reamer.
Boundary vs valve body / vs manifold
| Page | Owns |
|---|---|
| Hydraulic Valve Body Machining (#12) | Full valve-body feature map (spool · cavity · ports) |
| This page (#14) | Spool bore finishing — allowance, runout, ream path, RFQ |
| Hydraulic Manifold Drilling (#13) | Manifold intersecting / oil-passage drilling |
Bearing-bore analogies on EV / Al housings are soft only—do not steal those primary keywords: EV Motor Housing · Aluminum Housing Bearing Bore (sibling in this batch).
Milling appears only as support when a face lands on the same print—never as a second pillar on this URL.
RFQ fields for spool-bore finishing
| Must send | Why |
|---|---|
| Valve-body print/model + revision; spool bores marked | Separates finish lands from clearance |
| Hole chart: Ø, depth, tol, roundness/straightness if on print | Freezes drill vs ream scope |
| Pre-hole method + measured allowance / stock band | Incoming band before geometry freeze |
| Holder, stickout, measured runout, coolant | Trial realism |
| Material / alloy notes; volume band; sample yes/no + written acceptance | First-article before production talk |
Checklist: PCD Reamer RFQ Checklist. Quality soft: How PCD reamers are made · Manufacturing Quality Evidence.
Tool match pointers (short cards — not full catalog)
| Need | Open |
|---|---|
| Spool-bore finish | Custom PCD Reamer |
| Create-hole / pilot | Solid Carbide Drill |
| Step collapse (when print justifies) | Combination Drill-Reamer |
| Valve-body overall map | Soft → Hydraulic Valve Body Machining |
When does a spool bore need PCD reaming vs a carbide ream pass?
PCD reaming earns the station when the spool land is fit-critical (diameter/roundness/finish) on a compatible non-ferrous or abrasive aluminum route, and carbide edge life or finish drift becomes the limiter. Carbide ream may stay for looser lands or ferrous routes that do not justify PCD. Soft compare: PCD reamer vs carbide reamer. Mark critical spool lands and send material notes via Custom Cutting Tool RFQ.
What allowance should I leave before finishing?
Do not freeze a catalog stock number without measuring the pre-hole band. Allowance guidance lives on PCD reamer allowance & pre-hole size—this page does not invent a universal value. Send measured incoming Ø + intended stock with the RFQ.
How is this page different from hydraulic valve body machining?
Hydraulic Valve Body Machining owns the full valve-body path (spool · cavity · ports). This page owns spool bore finishing only—allowance, runout, PCD ream path, and RFQ fields. Use both: map the body on #12, finish the spool stack here.
What drawing fields do you need for a spool-bore RFQ?
Valve-body print with spool bores marked, hole chart (Ø, depth, tol, roundness/straightness callouts), pre-hole method and allowance, holder/runout/coolant, material notes, and which characteristics are in sample acceptance. Upload via Custom Cutting Tool RFQ. Checklist: PCD Reamer RFQ Checklist.
Send the valve-body print—we’ll map spool-bore allowance and ream
Mark spool lands on the print with measured pre-hole and runout. Engineering RFQ only—no public price list.