
High-Silicon Aluminum Housing Holes — PCD Path and RFQ
The carbide edge died on the housing bore before the batch ended—and the RFQ never named Si%. High-silicon aluminum scrap is usually an abrasive + allowance problem first, not a missing catalog SKU.
This page owns high-silicon aluminum housing hole application: why high-Si changes the tool call (short), housing path, RFQ with Si% required, and boundaries. Material science depth stays on Aluminum silicon content — PCD vs carbide and PCD reamer vs carbide reamer. High-speed application depth: PCD Aluminum High-Speed. XRZ quotes from your housing print plus Si% and bore stack (sample validation · Custom Cutting Tool RFQ).
Why high-Si changes the tool call (short — soft Knowledge)
| Signal | Heuristic (not a fake standard cutoff) |
|---|---|
| Rising abrasive Si in Al alloys | Carbide edge wear accelerates on finish bores |
| Tight diameter / roundness on housing fit bores | Finish often moves to PCD after controlled pre-hole |
| Unknown Si% on the RFQ | Quote risk — ask before freezing geometry |
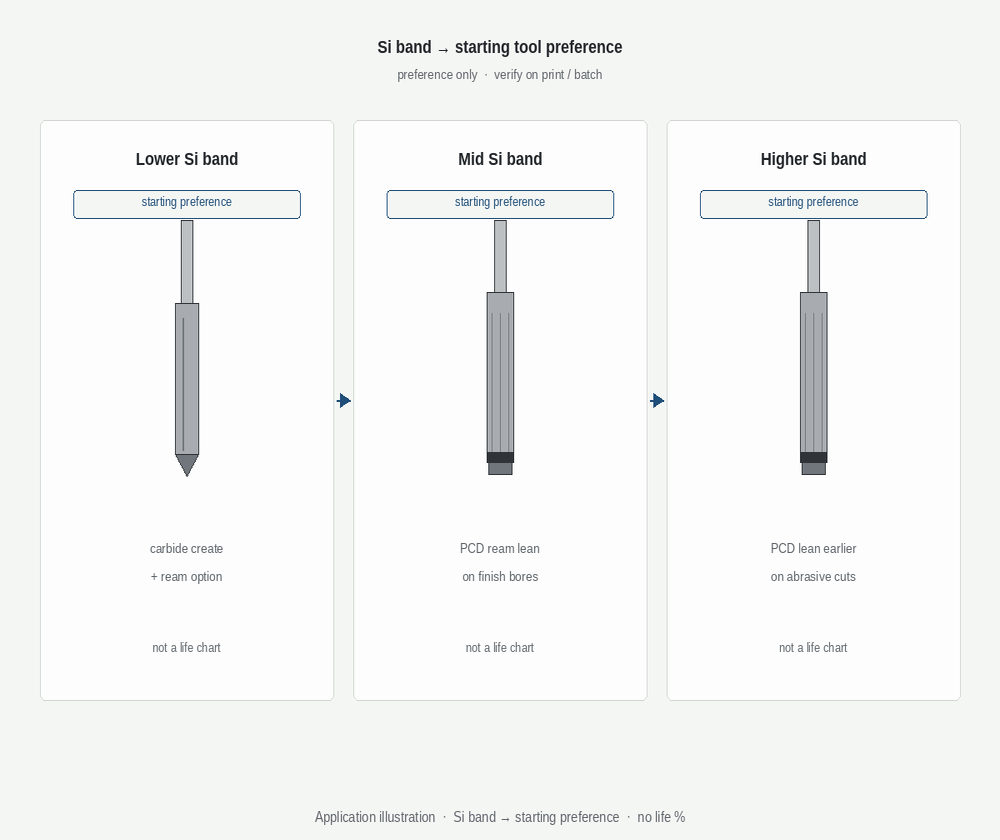
Do not restate Si% or vs-carbide H2s here. Soft: Si% guide · PCD vs carbide reamer. Heuristic only: mid-to-high Si bands often push fit bores toward PCD—never treat a single % as a universal plant standard without your print and process notes.
Application path on housings
- Create-hole — Solid Carbide Drill matched to Al chip/coolant reality.
- Measure incoming band; freeze allowance honestly — soft allowance Knowledge.
- Finish fit-critical bores with Custom PCD Reamer when Si abrasion + tolerance justify it.
Housing scene soft-links (do not paste): Aluminum EV Housings · EV Motor Housing · Aluminum Housing Bearing Bore.
RFQ: Si% required
| Must send | Why |
|---|---|
| Si% (or alloy designation + Si note) | First gate for PCD vs carbide discussion |
| Housing print + critical bores / bore chart marked | Freezes finish scope |
| Pre-hole method + measured allowance | Incoming band before geometry freeze |
| Holder, stickout, measured runout, coolant | Trial realism |
| Volume band + sample yes/no + written acceptance | First-article before production talk |
Checklist: PCD Reamer RFQ Checklist.
Soft-link Knowledge / #4 / housing scenes
| URL | Owns |
|---|---|
| Si% Knowledge | Material / Si% main |
| vs carbide | Compare main |
| PCD Aluminum High-Speed (#4) | High-speed Al PCD application |
| This page (#19) | High-Si housing hole application + RFQ |
Boundary: not every Al hole needs PCD
Clearance and non-gauge openings often stay on the carbide create-hole path even on high-Si cases. Mark finish-critical bores. Milling supporting only when a face lands on the same print—never a milling pillar here.
Tool match pointers (short cards)
| Need | Open |
|---|---|
| High-Si fit-bore finish | Custom PCD Reamer |
| Create-hole | Solid Carbide Drill |
| Material depth | Soft → Si% / vs-carbide Knowledge |
What Si% usually pushes a housing bore to PCD?
Heuristic only: as Si rises into mid-to-high bands, abrasive wear often pushes fit-critical housing bores toward PCD after a controlled pre-hole. There is no single universal cutoff published as a plant standard on this page—send your Si% / alloy and bore chart. Soft: Si% guide.
Is this the same as the PCD vs carbide reamer guide?
No. PCD vs carbide reamer owns the compare essay. This page owns the high-Si housing hole application and RFQ gate (Si% required).
Do I send Si% with every aluminum housing RFQ?
Yes when Si is known or the alloy is Al-Si—especially for finish-critical bores. Unknown Si% raises quote risk. Upload via Custom Cutting Tool RFQ.
How does this page differ from the high-speed aluminum PCD page?
PCD Aluminum High-Speed owns high-speed Al PCD application depth. This page owns high-Si housing holes + RFQ Si%—not a second high-speed parameter encyclopedia.
Send the housing print with Si%—we’ll map PCD ream paths
Put alloy/Si% and critical bores on the RFQ. Engineering quote only—no public price list.