
Compressor Housing Machining — Bores, Tools, RFQ
The housing RFQ still asked for “compressor tools” while the print marked bearing bores, locating diameters, and oil galleries that do not share one flute story—and the scroll-plate page does not own this case.
This page owns compressor housing bore machining: housing hole map, short Al vs ferrous fork, tool match, and RFQ. Scroll-plate / orbiting-disk work stays on Aluminum Scroll Compressor Plate Machining. Industry context: Automotive Powertrain. XRZ quotes from your housing print with critical bores marked (sample validation · Custom Cutting Tool RFQ).
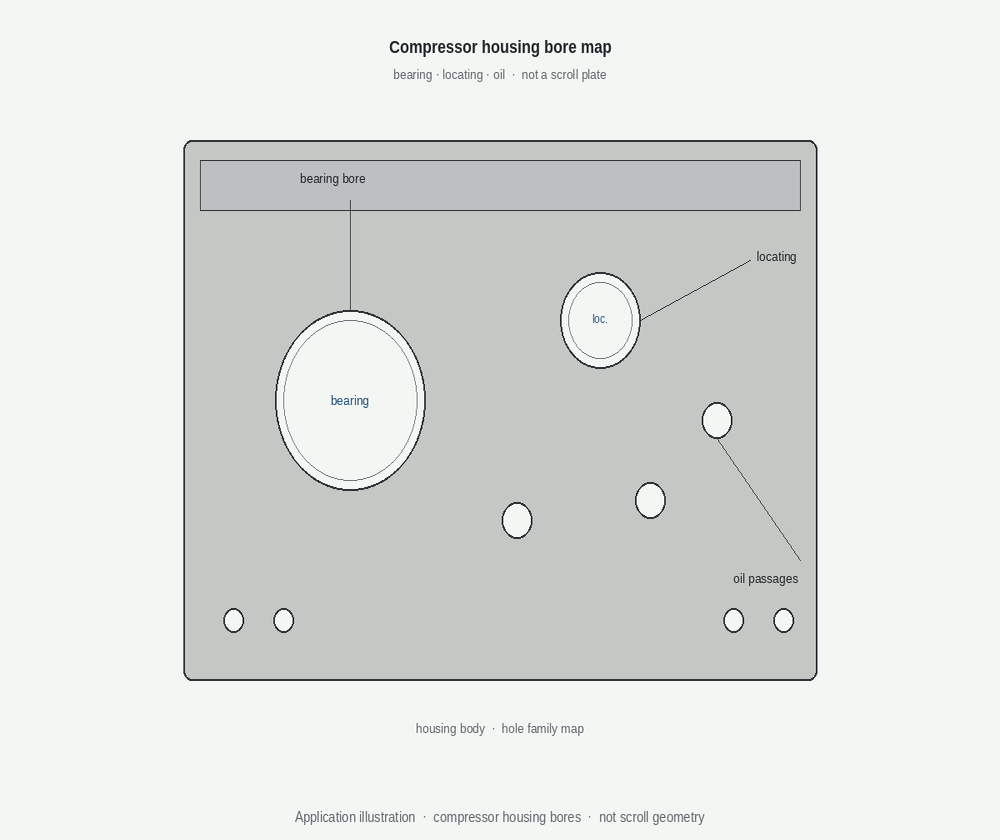
Housing bore map
| Feature | What usually drives tooling |
|---|---|
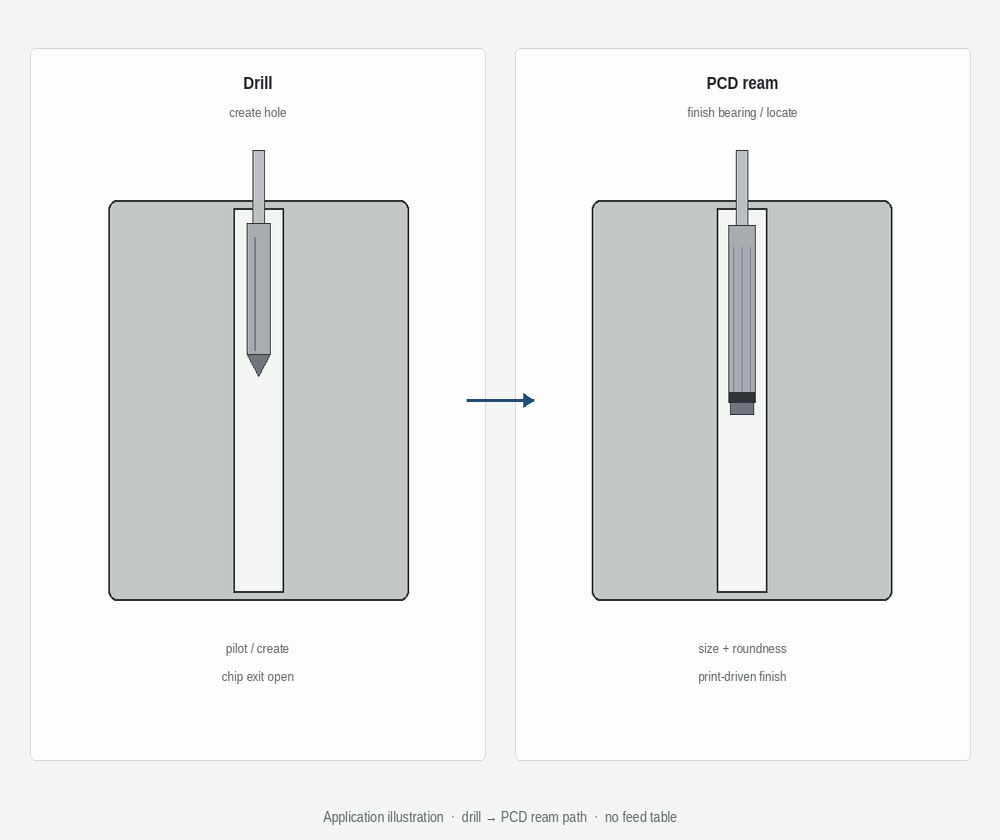
| Bearing / main fit bores | Diameter, roundness, alignment → often drill → measure → PCD ream |
| Locating / register diameters | Position + fit; ream when gauge requires |
| Oil / coolant / vent holes | Create-hole + chip/burr plan; ream only when print demands |
| Coaxial / multi-diameter stacks | Treat as one alignment problem — soft EV Housing Coaxial Bore Machining (sibling) |
Do not expand into a scroll-plate encyclopedia—soft Aluminum Scroll Compressor Plate Machining.
Aluminum vs ferrous (short fork)
| Material fork | Typical holemaking posture |
|---|---|
| Aluminum / Al-Si housings | Carbide create-hole + PCD ream on fit-critical bores; send Si% when known |
| Ferrous / cast-iron cases | Carbide drill primary; ream only where print + gauge justify—do not default every bore to PCD |
Soft material depth (do not restate): Aluminum silicon content — PCD vs carbide · PCD reamer vs carbide reamer. High-Si housing application: High-Silicon Aluminum Hole Machining (sibling).
Tool cards (short — not full catalog)
| Need | Open |
|---|---|
| Fit-bore finish | Custom PCD Reamer |
| Create-hole | Solid Carbide Drill |
| Cycle collapse when print justifies | Combination Drill-Reamer |
Combination tools earn a station when cycle time and capability justify collapsing steps—not as a default housing slogan. Soft: Drill-then-ream vs PCD combination.
Soft boundaries (siblings)
| Page | Owns |
|---|---|
| Scroll plate machining (#5) | Scroll / plate features |
| This page (#15) | Compressor housing bore map + RFQ |
| Pump Housing Bearing Bore (#16) | Pump bearing scene |
| EV Housing Coaxial Bore Machining (#18) | Coaxial / multi-diameter depth |
Milling appears only as support when a face lands on the same print—never as a second pillar on this URL.
Housing RFQ pack
| Must send | Why |
|---|---|
| Housing print/model + revision; critical bores marked | Separates finish bores from clearance |
| Hole chart: Ø, depth, tol, alignment/coaxial callouts if on print | Freezes drill vs ream scope |
| Material / alloy + Si% when Al | Wear and edge discussion—not a life promise |
| Pre-hole method + allowance for finish bores | Incoming band before geometry freeze |
| Machine, holder, stickout, measured runout, coolant | Trial realism |
| Volume band + sample yes/no + written acceptance | First-article before production talk |
Checklist: PCD Reamer RFQ Checklist.
How is compressor housing machining different from scroll plate machining?
Aluminum Scroll Compressor Plate Machining owns scroll / plate features. This page owns the housing case bore map—bearing, locating, oil/coolant—and the RFQ for those holes. Use the scroll page for plate work; send housing prints here.
Do all compressor housing bores need PCD reaming?
No. PCD reaming belongs on fit-critical bearing and precision bores after a controlled pre-hole. Clearance and non-gauge openings often stay on the carbide create-hole path. Mark critical bores and send material notes via Custom Cutting Tool RFQ · product Custom PCD Reamer.
When is a combination drill-reamer useful on a housing?
When cycle time and process capability justify collapsing create-hole and finish on a diameter the print allows—not as a default for every housing bore. Soft: Drill-then-ream vs PCD combination · Combination Drill-Reamer.
What should I send for a compressor housing RFQ?
Housing print with critical bores marked, hole chart, material/Si% when Al, pre-hole/allowance for finish bores, holder/runout/coolant, and sample acceptance list. Upload via Custom Cutting Tool RFQ.
Send the housing print—we’ll map bearing, locating, and oil bores
Mark critical bores on the compressor housing print. We quote from material fork and machine constraints.