
Product Detail
Micro End Mills for Precision Milling
Confirm size, tip style (flat/ball/corner radius), geometry, runout, and chip exit, then send a drawing for micro end mill RFQ.

Micro milling · solid carbide
Micro End Mills for Precision Milling
Confirm size, tip style (flat/ball/corner radius), geometry, runout, and chip exit, then send a drawing for micro end mill RFQ.
- Lock diameter and tip style before flute length or neck
- Match material geometry to chip load and entry strategy
- Review runout and chip exit before production RFQ
Small-diameter sizes
Confirm cutting diameter and shank before tip style. Unconfirmed stock diameters are not listed as standard range, blank cells mean to your drawing. Broader milling tools stay on carbide end mills and micro precision.
Cutting Ø first
Match the print, do not round to a “close” catalog row. State tolerance if the feature is critical.
Holder interface
Collet, shrink, or hydraulic, state holder type and available projection. Runout review follows.
Flute vs overall
Separate flute length from overall length and neck. Depth of cut does not equal flute length by default.
Flat, ball, and corner-radius tips
Tip style is a separate decision from diameter. Cards below keep names aligned with photos.
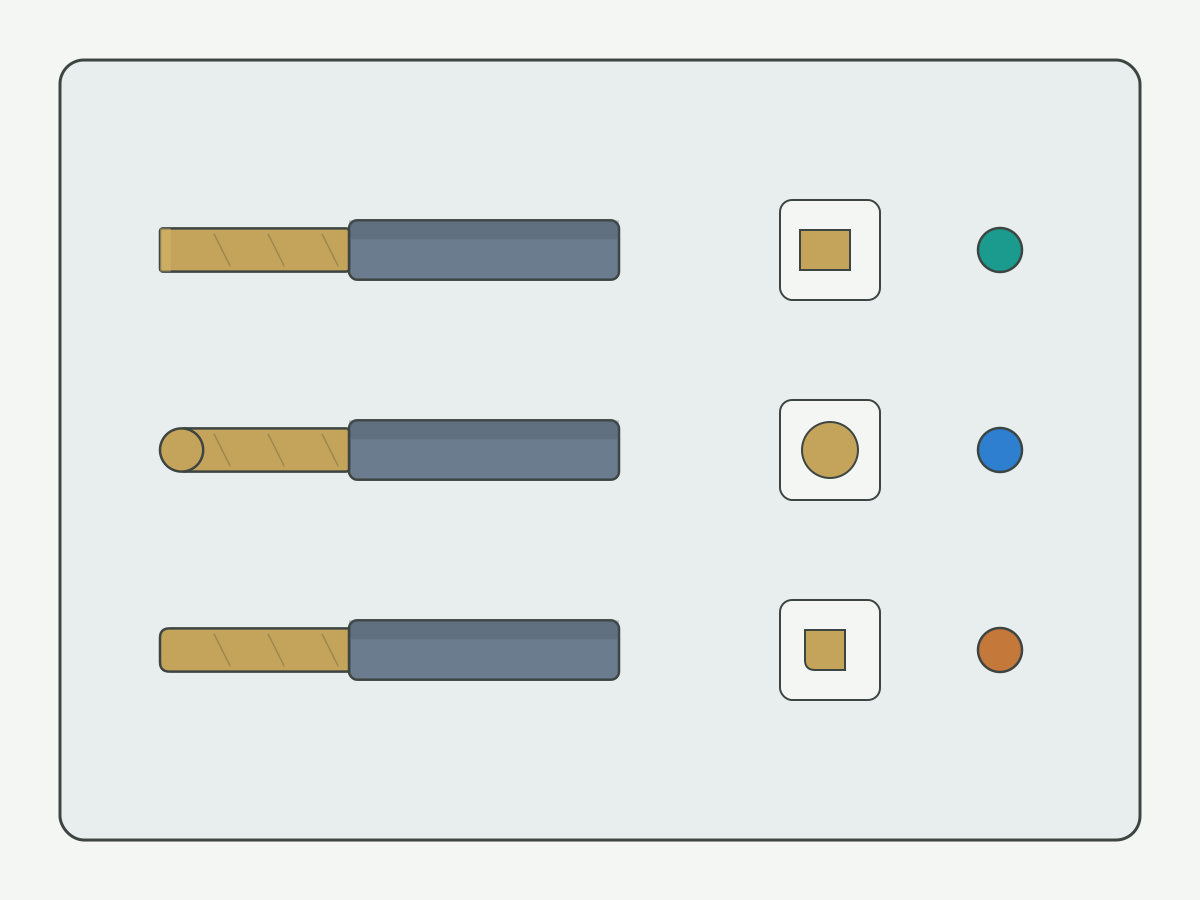
- Flat / square Sharp corner or small land. Confirm whether a sharp corner is allowed on the print.
- Ball Full-radius tip for 3D or fillet work. State ball Ø separately from shank.
- Corner radius Defined R on a flat tip. Send R value, do not infer from ball mill stock.
- Support reading General milling taxonomy on the milling tools guide.
Material geometry and flute length
Geometry and flute length follow material and feature depth, not a single “micro” default.
| Input | Why it matters | If unknown |
|---|---|---|
| Workpiece material | Sticky vs hard vs abrasive changes flute and coating needs | Alloy / condition · to your drawing |
| Flute length | Must clear depth of cut with chip space | Feature depth + stock allowance |
| Neck / reach | Wall clearance without confusing flute length | Reach and interference sketch |
| Coating / substrate | Application-dependent, not a universal upgrade | State preference only if required |
Runout, entry, and chip evacuation
Micro tools fail early when tip TIR, entry strategy, or chip packing is ignored.
Products and custom RFQ
Upload a feature section when possible. Engineering confirms size, tip, and runout before locking a series.
- Known series + print: send both for cross-check and supply confirmation.
- Only a workpiece print: send material, Ø, tip style, depth, and holder type for preliminary selection.
- Quotation timing: after complete drawing information, quotation typically takes 1–2 working days (quotation only).
Selection guide
One row per task. Empty numeric cells mean confirm from drawing, not zero.
| Task | Size Ø | Tip | Flute length | Material | Next |
|---|---|---|---|---|---|
| Flat slot / pocket | to your drawing | Flat / square | to your drawing | Alloy / condition | RFQ |
| 3D / fillet | to your drawing | Ball | to your drawing | Alloy / condition | RFQ |
| Corner-blend wall | to your drawing | Corner radius · to your drawing | to your drawing | Alloy / condition | RFQ |
| Deep / long reach | to your drawing | Per print | Neck + flute · confirm | Runout review | RFQ |
Blank cells are intentional. Unconfirmed series dimensions are not shown as “standard range.”
Micro end mill FAQ
Answers state decision conditions and next steps. They do not replace application approval.
Which tip style should I choose?
Match the print: flat/square for sharp corners, ball for full-radius 3D or fillets, corner radius when a defined R is specified. Do not substitute a ball mill for a corner-radius callout without engineering review.
What sizes should I send on the RFQ?
Cutting diameter, tip style (and R if any), flute length or feature depth, shank/holder type, material, and runout target if known. Blank catalog cells mean confirm from drawing.
How critical is runout on micro end mills?
Very. Tip TIR drives size and tool life assumptions. State holder type and inspection method. Unverified runout claims are not published as stock specs.
Why is there no public stock list or price?
HENTRY quotes from application data and approved supply scope. Quotation typically follows within 1–2 working days after complete drawing information.
Send a Micro End Mill Drawing
Page N007 · Product Micro End Mills for Precision Milling. Required: email, product or task, requirement description. Optional: drawing upload, company, material, sizes, machine, quantity. "Model uncertain" is allowed.
Footer / legal entity: Guangdong Hentry Tool Technology Co., Ltd Brand on page: HENTRY.