
Product Detail
Cutting Inserts for CNC Turning
Compare available insert families and provide your workpiece, operation, and holder details for an application review.
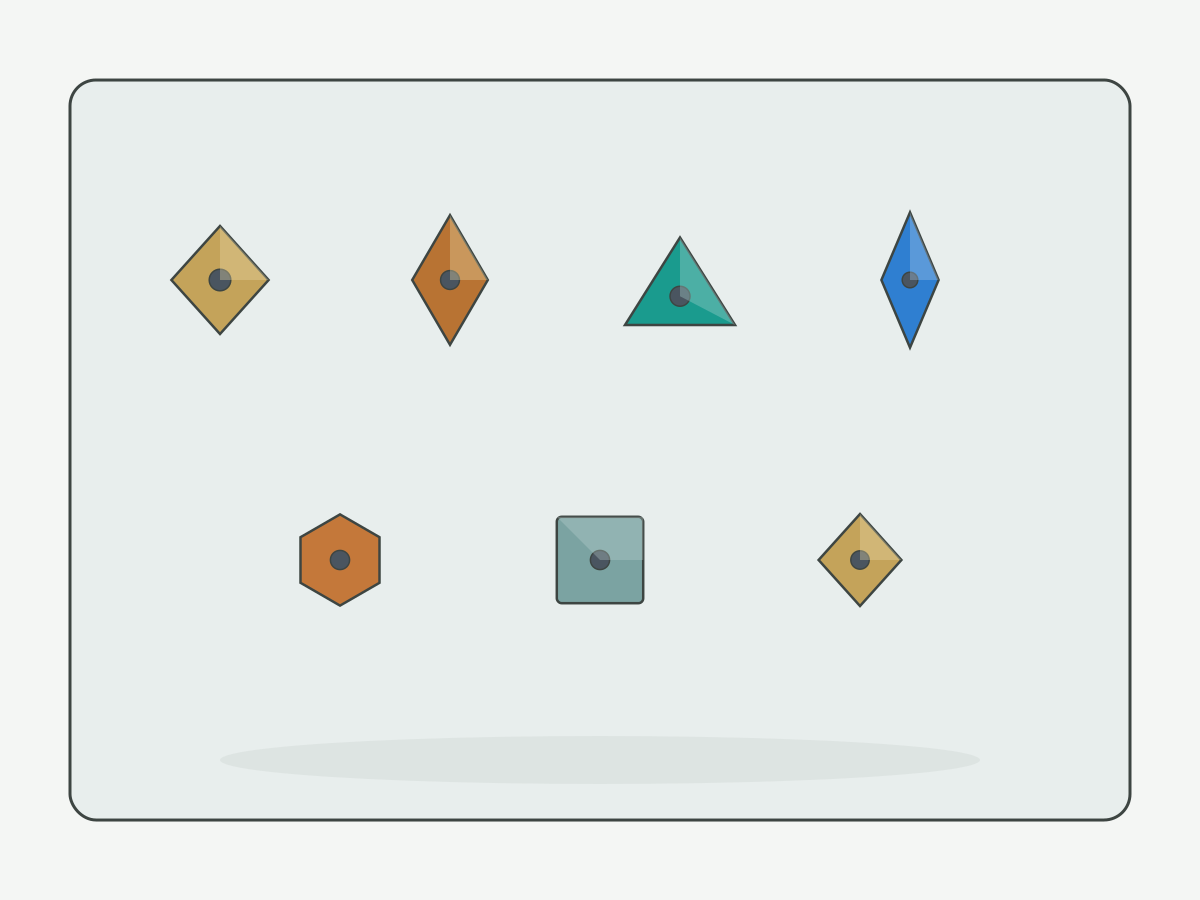
Cutting inserts · CNC turning
Cutting Inserts for CNC Turning
Compare available insert families and provide your workpiece, operation, and holder details for an application review.
- Tungsten carbide inserts are the primary entry on this page
- PCD and CBN routes stay on planned child pages when supply is confirmed
- Holder pocket and duty data are required before a firm match
Insert material and families
Start with the cutting material family that matches the workpiece and duty. This hub does not delete planned PCD/CBN pages; it keeps carbide as the clear tungsten-carbide entry.
Carbide turning inserts
General steels, cast irons, and many stainless applications. Grade, chipbreaker, and edge prep are confirmed from your operation — not from a single material name.
Request carbide insert reviewPCD turning inserts
Non-ferrous / aluminum high-volume paths when PCD supply is confirmed. Not a drop-in for ferrous work.
Review our PCD turning inserts product information and share your application requirements.
PCD turning insertsCBN / PCBN inserts
Hardened ferrous finishing routes when CBN supply is confirmed. Interrupted-cut limits must be reviewed.
Review our CBN and PCBN inserts product information and share your application requirements.
CBN / PCBN insertsShape and ISO designation
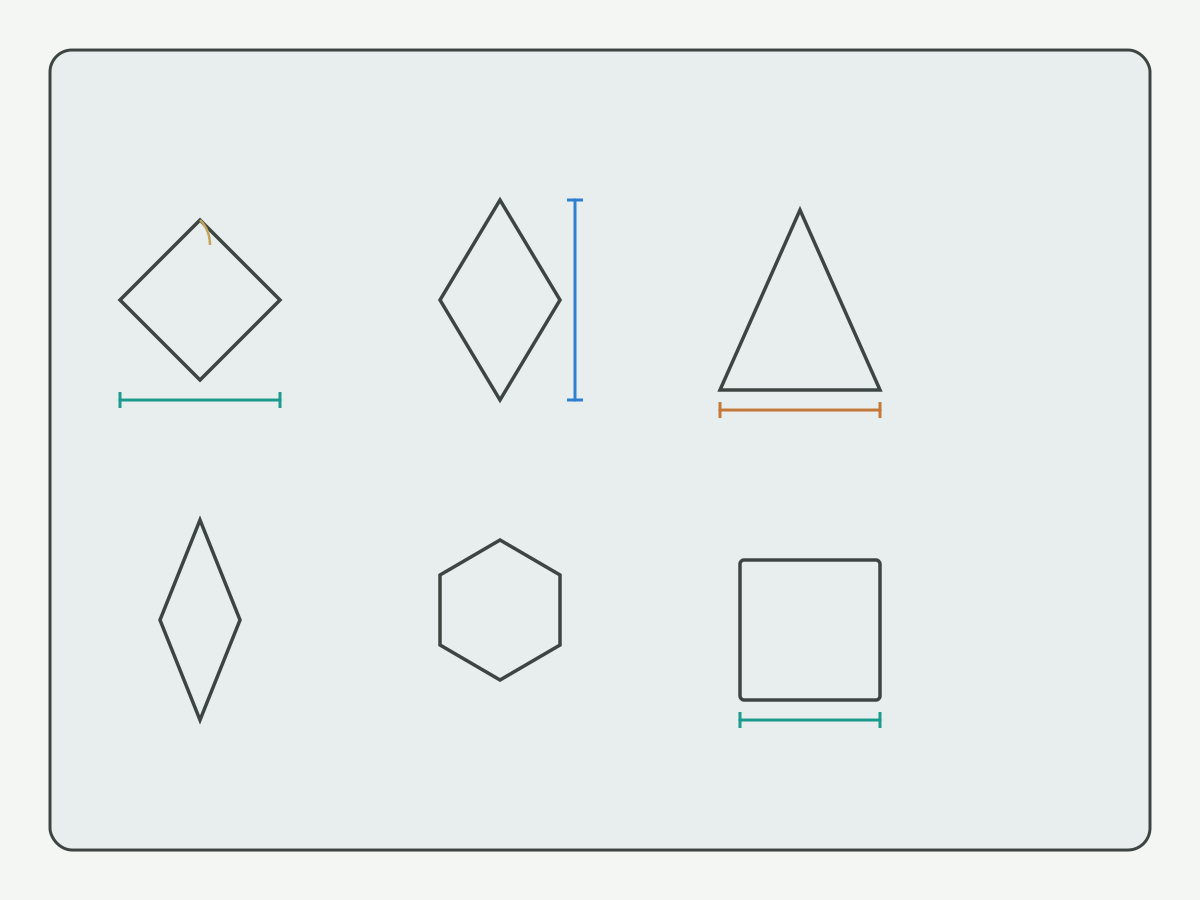
ISO insert codes encode shape, clearance, tolerance, type, size, thickness, and nose radius. Only engineering-approved examples are shown with version notes. Unconfirmed standard sizes are not filled in.
How to use a code
If you have a full designation: send it for cross-check and supply confirmation.
If the code is incomplete: send a clear photo of the insert faces, thickness, hole, and the holder pocket — or the workpiece print for application selection.
Decode example block: 按图纸 / engineering-approved sample pending. Do not invent a fake CNMG example as “our standard.”
Workpiece material match
Every row needs operation mode and confirmation items. A material name alone is not an applicability claim.
| Workpiece direction | Operation mode | First-pass family | Must confirm |
|---|---|---|---|
| Carbon / alloy steel | Continuous or light interrupt | Carbide | Chip control, coolant, speed band |
| Cast iron | Continuous / abrasive | Carbide | Edge wear, dust, rigidity |
| Stainless | Often heat + work-hardening | Carbide (review) | Feed, edge prep, interrupt |
| Aluminum / non-ferrous | High volume / abrasive | Carbide or PCD route | Built-up edge, volume |
| Hardened ferrous | Finish / hard turn | CBN route (if supplied) | Hardness, interrupt, machine |
Holder compatibility
Compatibility lists only come from real catalogs or supplier confirmation. Same insert outline does not prove interchange across brands.
Checklist before RFQ
- Pocket style and clamping (screw / lever / wedge)
- Insert thickness and hole / without hole
- Hand of cut and approach orientation
- Clearance to workpiece and turret
Two RFQ paths
Existing insert designation
Send the full code (or photo). Cross-brand matches are treated as candidates until verified — not as guaranteed drop-ins.
Replace-by-code RFQNew workpiece / operation
Send material, OD/ID/face feature, tolerance, continuous vs interrupted, and holder interface. Quotation typically 1–2 working days after complete drawing info.
Application RFQTurning tools overview
Need holders, boring bars, or feature routing first? Start at the turning tools hub.
Open turning toolsSelection guide
| Family | Insert material | Shape / size | Edge / chipbreaker | Duty | Holder | Status |
|---|---|---|---|---|---|---|
| Carbide turning | Tungsten carbide | 按图纸 / code | Engineering review | Steel / CI / SS review | Pocket match required | RFQ · primary |
| PCD turning | PCD | When supplied | Application review | Non-ferrous gates | Dedicated holders | Day2 planned |
| CBN / PCBN | CBN | When supplied | Application review | Hard ferrous gates | Dedicated holders | Day2 planned |
Blank numeric cells are intentional. No invented stock catalog.
Cutting inserts FAQ
Can you replace my current insert code?
Send the full designation or a clear photo. We verify supply and holder pocket compatibility. Unverified cross-brand codes are evaluation inputs only.
Where do I compare PCD vs carbide?
Carbide is the primary path on this page. PCD and CBN child pages are planned for Day2. Until they are live, state material and volume in the RFQ so engineering can route the family.
What if I do not have a complete ISO code?
Send workpiece material, operation (OD/ID/face), continuous vs interrupted, holder photos or interface, and the drawing. Application selection does not require a perfect code on day one.
Why are grades not listed as a full public matrix?
Unapproved grades are not published as standard range. HENTRY quotes from confirmed supply and your duty data after drawing review.
Request Insert Selection
Page N004 · Product Cutting Inserts for CNC Turning. Email, task, and requirement description required; drawing optional.
Guangdong Hentry Tool Technology Co., Ltd · Brand: HENTRY