
This page helps CNC process engineers, programmers, and tooling buyers lock a tap drill size for 1/4-20 UNC and 1/4-28 UNF: separate the 1/4-inch major diameter from the 20 versus 28 TPI callout, read the common cut-tap chart rows (#7 for 1/4-20 and #3 for 1/4-28 at about 75 percent engagement on many public charts), keep form-tap prep holes and bolt clearance holes off the cut-tap row, then confirm with the drawing class and tap maker chart before RFQ. The live multi-system hub stays on the tap drill size chart. This page is the 1/4-inch 20/28 OWN; it is not a full metric/UNC/UNF encyclopedia, a 5/16 page, a 10-32 page, a bolt clearance-hole chart, a form-versus-cut encyclopedia, or an invented ranking, price, life claim, or unsourced size matrix.
Start from the live form tap vs cut tap guide when method (form versus cut) is still open. Browse live constructions on taps and carbide drill bits. When a thread mill may replace tapping, use the live thread milling vs tapping aluminum guide and browse thread mills. Hole-process framing sits on the live precision holemaking selection guide. Sister deep dives for 5/16 and 10-32, plus a bolt clearance-hole chart, will be linked after they publish (soft-note until live). End with RFQ when the package is ready: custom cutting tool RFQ.
Quick answer
- Lock major size and TPI before any drill letter: "1/4" alone is not enough. Write 1/4-20 UNC (coarse, 20 threads per inch) or 1/4-28 UNF (fine, 28 TPI) on the traveler. Swapping TPI while keeping the same major diameter is how the wrong chart row gets used.
- 1/4-20 cut-tap starter (public chart consensus ~75% engagement): many published UNC cut-tap charts list a #7 drill (0.2010 inch). Treat that as chart consensus, not an HC laboratory measurement. Confirm drawing class, material, and the tap maker chart before production.
- 1/4-28 cut-tap contrast: many published UNF cut-tap charts list a #3 drill (0.2130 inch) near the same ~75% basis. Do not reuse the #7 from the 1/4-20 row. Fine pitch leaves less material to remove at the same major diameter, so the cut-tap drill is larger.
- Form tap and clearance stay off the cut-tap row: a form (roll) tap needs a larger prep hole from the maker chart; a bolt clearance hole is intentionally larger so the shank passes and is not a tap drill. Next step: name material, hole type, cut versus form, and drill with units, then open RFQ if needed.
Selection path (stop when a field is missing):
| Step | What you lock | If missing |
|---|---|---|
| 1 Major + TPI | 1/4-20 UNC or 1/4-28 UNF (or reject other 1/4 callouts) | Stop; recover the print callout |
| 2 Method | Cut tap, form tap, or open; ductility note | Do not pick a drill from habit alone |
| 3 Percent of thread / class | Target engagement or thread class and check method | Keep drill open; do not invent a % |
| 4 Prep-hole size | #7 / #3 (or maker form size) + decimal inch + chart family | Do not tap from a clearance hole |
| 5 Material and hole type | Grade/condition, blind vs through, depth, interruptions | Escalate before production |
| 6 Trial and RFQ | First-off gauge result + matched RFQ package | Open RFQ with incomplete SKU if needed |
Jump: 1/4 vs TPI · 1/4-20 cut-tap · 1/4-28 contrast · Form and clearance · Worked examples · RFQ · Confirm · FAQ
Distinguish 1/4-inch major diameter from 20 and 28 TPI
Shop slang that says "a quarter-inch tap" without TPI is incomplete. Unified inch geometry names both the major diameter and the threads-per-inch series. Unified naming literacy is framed in the ASME B1.1 family; use public standards literacy such as this codes and standards portal for naming only, not as a pasted B1.1 substitute.
- 1/4-inch major diameter: the nominal major size is 0.250 inch for both 1/4-20 and 1/4-28. That shared major is why teams confuse the two rows.
- 1/4-20 UNC: Unified National Coarse at 20 TPI. Common on general mechanical fasteners. Coarse pitch removes more material for a given major diameter, so the cut-tap prep hole is smaller than the matching fine row.
- 1/4-28 UNF: Unified National Fine at 28 TPI. Common when a finer pitch is specified for adjustment, thin wall, or vibration-sensitive stacks. Fine pitch needs a larger cut-tap drill than 1/4-20 at the same major.
- Not this page's OWN: other 1/4 callouts (for example special pitches), metric M6 near-size swaps, 5/16 deep dives, 10-32 deep dives, NPT, and bolt clearance-hole fit classes belong elsewhere. The multi-system starter tables stay on the live tap drill size chart.
Public screw tables such as this laboratory UNC/UNF screw table help teams name size and TPI side by side. Metrology literacy such as this public metrology laboratory entry and this weights and measures overview supports keeping inch decimals honest on the traveler. Unit conversion literacy such as this NIST SP 811 units guidance and this NIST SP 811 publication PDF supports inch/mm discipline when a shop also holds metric taps.
1/4-20 UNC cut-tap drill (public chart consensus)
For a cut tap on 1/4-20 UNC, many published shop charts list a #7 drill at 0.2010 inch, aimed at roughly 75% of full thread for general mechanical work. That percent-of-thread basis is a shop convention used on many public charts; it is not a universal strength guarantee and not an HC measured result for every grade.
Source boundary: ASME B1.1-style Unified inch cut-tap chart practice as reflected in public UNC tap-drill references (cross-checked against consolidated public charts such as this UNC UNF and metric tap drill chart and this tap drill reference table). Engineering applicability: cut taps only; ductile or free-cutting materials at commercial thread targets; blind or through holes when chip exit is planned. Verify against the drawing thread class and the tap maker chart before production. Charts can disagree by one stock size; when they do, prefer the print and the tap maker over habit.
| Thread | Series | TPI | Typical cut-tap drill | Decimal (in) | Approx. basis | Confirm when… |
|---|---|---|---|---|---|---|
| 1/4-20 | UNC | 20 | #7 | 0.2010 | ~75% cut-tap chart consensus | Form tap, hard material needing lower %, or maker chart differs |
CNC threading literacy such as this CNC threading and tapping overview and this tap drill chart sizes overview frames percent-of-thread talk without turning this page into a feeds library. Public distributor help such as this tap drill sizes help page is literacy only, not an HC trial. Threading education such as this threading knowledge overview and this tapping knowledge overview adds process naming only (neutral anchors; not a brand ranking).
Common process notes for the 1/4-20 cut-tap path:
- Blind holes: leave unused depth for the tap chamfer; chip packing is a frequent break cause on 20 TPI coarse flutes when coolant or pecking is weak.
- Hard or tough alloys: shops often move toward a slightly larger drill (lower %) to protect the tap. That is a conditional trade, not a free strength upgrade. Do not invent a life percentage as an HC result.
- Soft aluminum: a #7 cut-tap row may still be appropriate, but if the method flips to form tapping, abandon the #7 and use the form maker window instead.
- Gauge the finished thread to the print method. Class labels and percent-of-thread talk are related but not interchangeable.
1/4-28 UNF cut-tap contrast (same major, different drill)
For a cut tap on 1/4-28 UNF, many published shop charts list a #3 drill at 0.2130 inch, again near a ~75% engagement convention on public charts. The major diameter is still 0.250 inch; the finer pitch is why the prep hole grows relative to 1/4-20.
Source boundary: same ASME B1.1-style Unified inch cut-tap chart family and public UNF tap-drill consensus as the 1/4-20 row above. Applicability: cut taps; commercial ~75% target; verify class and maker chart. This compare is conditional on cut method and a named engagement basis. It is not an unconditional ranking that "fine is better" or that #3 always wins.
| Thread | Series | TPI | Typical cut-tap drill | Decimal (in) | Approx. basis | Confirm when… |
|---|---|---|---|---|---|---|
| 1/4-20 | UNC | 20 | #7 | 0.2010 | ~75% cut-tap chart consensus | Print is actually 1/4-28; form method; hard material |
| 1/4-28 | UNF | 28 | #3 | 0.2130 | ~75% cut-tap chart consensus | Print is actually 1/4-20; form method; thin wall / class shift |
How to read the contrast: at the same 0.250 inch major, moving from 20 TPI to 28 TPI reduces the material that must be removed for a given engagement target, so the published cut-tap drill steps up from #7 (0.2010 in) to #3 (0.2130 in). Reusing #7 on a 1/4-28 callout is a common mix-up when the traveler only says "1/4". Reusing #3 on a 1/4-20 callout leaves the thread under-engaged relative to the chart intent.
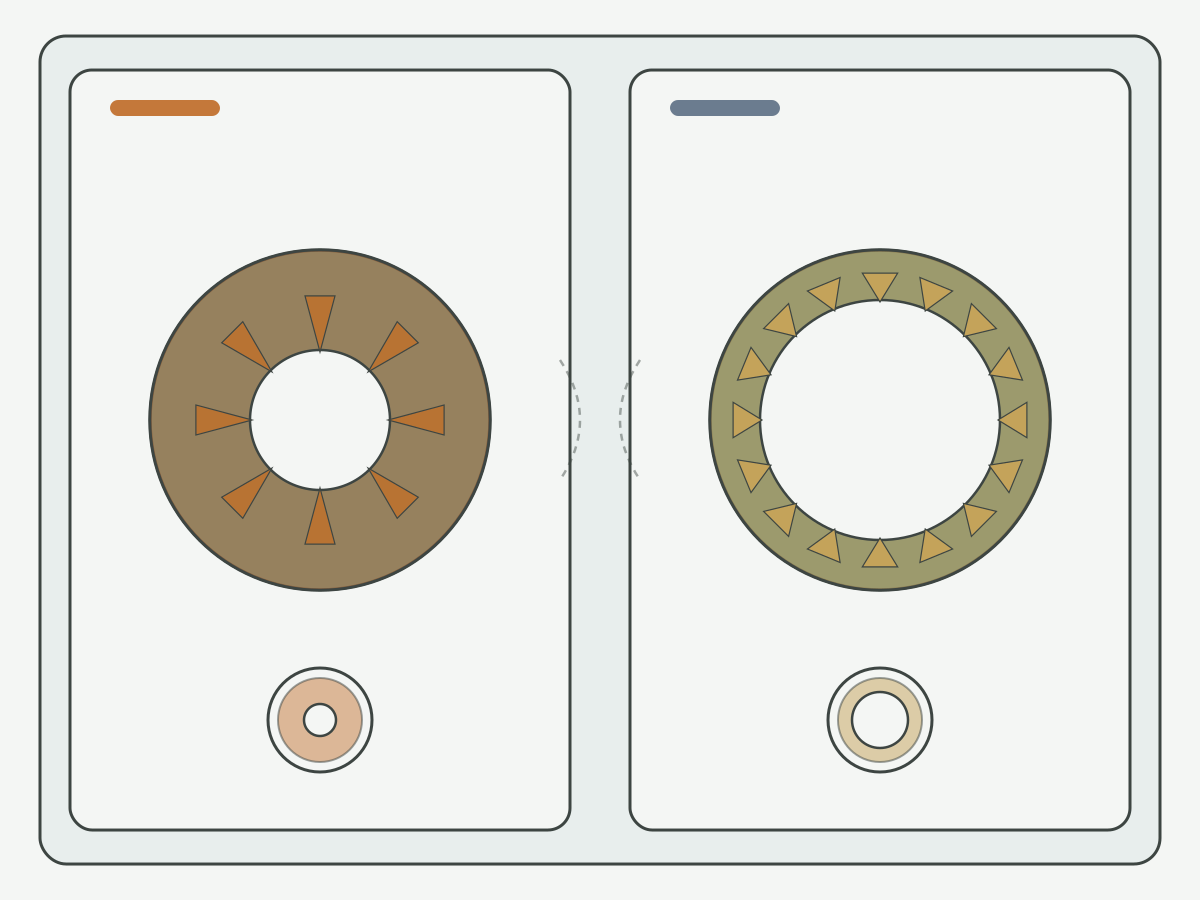
Schematic illustration: not a catalogue ranking or cutting-data table. Confirm TPI, drill diameter, percent-of-thread target, and cut versus form on your drawing and tap maker chart.
National standards literacy such as this national standards overview supports naming thread families only. Engineering calculator literacy such as this engineering calculators portal helps name engagement math without inventing HC life data.
Form-tap prep holes and clearance holes (not the cut-tap row)
Two other hole sizes get confused with 1/4-20 and 1/4-28 tap drills. Keep them on separate traveler lines.
- Form (roll / cold-form) taps: material displaces into the thread form, so the prep hole is larger than the cut-tap #7 or #3 for the same nominal callout. Reusing a cut-tap drill on a form tap often causes swell, incomplete crests, or excess torque. Choose method first on the live form tap vs cut tap guide, then use the tap maker form-drill chart for the SKU you will run.
- No invented form matrix here: this page does not paste a universal letter/number matrix for 1/4 form taps as an HC measured guarantee. Maker charts differ by geometry, coating, and material window. Prefer "confirm with tap maker / drawing" over an unsourced cell.
- Ductility and lubrication gates: industry tendency favors form taps on ductile workpieces (many aluminum alloys, low-carbon steels, some stainless grades) and cut taps on brittle or hard-to-form materials (many cast irons, some hardened conditions). Forming usually needs a robust lubricating film; cut tapping often prioritizes chip wash. Grade certificates beat nicknames.
- Bolt clearance holes: a clearance hole is intentionally larger so the bolt shank passes freely without engaging threads in that plate. Clearance is not a tap drill. Do not tap a clearance hole and call it 1/4-20 or 1/4-28 prep. A dedicated clearance-hole chart (planned path
/resources/bolt-clearance-hole-chart) will cover fit classes after it publishes (soft-note until live).
| Axis | 1/4 cut-tap tendency | 1/4 form-tap tendency | Bolt clearance tendency | Keep open when… |
|---|---|---|---|---|
| Hole size vs major | Smaller core (#7 or #3 by TPI) | Larger prep than cut row | Larger still; shank passes | Maker form chart or fit class missing |
| % thread / fit talk | Often ~75% on public cut charts | Maker-specific mid band | Close / normal / loose fit classes | Acceptance method unnamed |
| Material | Broader, including brittle grades | Needs ductility to flow | Plate stack / coating notes | Certificate grade unknown |
| RFQ note | State cut + TPI + #7/#3 | State form / roll + maker size | State clearance, not tap drill | Method or hole intent undecided |
This compare table is conditional. It is not an unconditional ranking of form over cut, of 28 TPI over 20 TPI, or of any brand. Fastener mechanics literacy such as this bolt science portal supports naming engagement talk without inventing case counts.
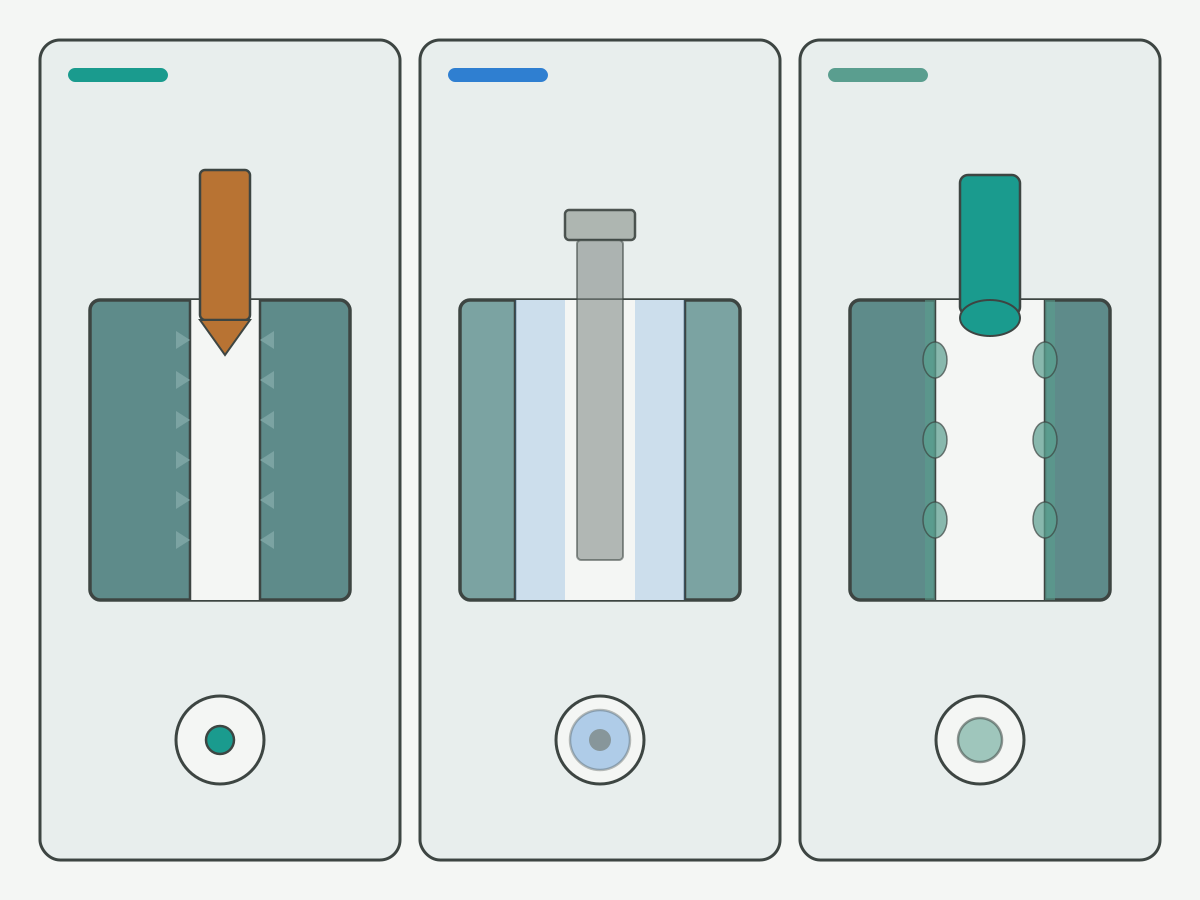
Schematic illustration: boundaries only, not a catalogue ranking. Confirm tap-drill versus clearance versus form-prep intent on the drawing before picking a drill.
Toolholding literacy such as this tool holder technology overview and cutting-data literacy such as this cutting data notes portal support naming sync tapping and holder stiffness beside drill choice. Research society literacy such as this CIRP research portal frames process research boundaries only.
Worked examples (1/4-20 intent gates)
These examples answer common search intents at dedicated-page depth. Each still needs drawing class and maker confirmation before production. They are teaching aids, not shop results.
| Intent example | Callout to lock | Common cut-tap starter | Page note |
|---|---|---|---|
| 1/4-20 tap drill size | 1/4-20 UNC | #7 (0.2010 in) | ~75% public chart consensus; verify maker |
| Bit size for 1/4 20 tap | 1/4-20 UNC | #7 (0.2010 in) | Write TPI; "1/4" alone is incomplete |
| Drill bit size to tap 1/4 20 | 1/4-20 UNC + cut method | #7 (0.2010 in) | Form method abandons #7 |
| 1/4 20 drill size for tap | 1/4-20 UNC | #7 (0.2010 in) | Do not use #3 from the 28 TPI row |
| 1/4-28 tap drill (contrast) | 1/4-28 UNF | #3 (0.2130 in) | Same major; larger cut-tap drill |
| Form tap on 1/4-20 or 1/4-28 | Same callout + form method | Larger than cut-tap row | Maker form chart only; no invented matrix |
| Clearance for 1/4 bolt (not tap) | Clearance fit class | Not #7 / not #3 as tap drill | Soft-note clearance chart until live |
Source boundary: same cut-tap chart families as the tables above (ASME B1.1-style / public UNC-UNF consensus at ~75%). Form and clearance rows stay qualitative. Soft-noted sister paths until live: 5/16 deep dive (/resources/5-16-tap-drill-size), 10-32 deep dive (/resources/10-32-tap-drill-size), bolt clearance-hole chart (/resources/bolt-clearance-hole-chart).
| Boundary | Lock on the sheet | Fail signal | Do not invent |
|---|---|---|---|
| TPI / series | 1/4-20 UNC or 1/4-28 UNF | Wrong engagement or gauge fail | Fake "universal 1/4 drill" |
| % thread / class | Target and check method | Gauge fail or tap break | Fake strength % as HC data |
| Material | Grade, condition, ductility note | Torn crests, swell, break | Life % from grade slang |
| Hole type / depth | Blind/through, unused depth | Chip pack or incomplete form | Price or ROI from depth |
| Drill vs clearance vs form | Named intent on traveler | Loose bolt or missing thread | Unsourced form letter matrix |
Procurement checklist (RFQ inputs)
Send what you know. Leave life, price, and unverified cycle-time fields blank. Do not invent an unconditional best-drill ranking for 1/4-20 versus 1/4-28.
- Drawing revision and thread callout (1/4-20 UNC or 1/4-28 UNF, class if known).
- Cut tap, form tap, or open method; ductility note if known.
- Percent-of-thread or engagement target and how it will be checked.
- Proposed tap-drill size with units (#7 / #3 and/or decimal inch) and chart family used; for form taps, maker form size instead of the cut row.
- Material grade, condition, and coolant or forming-oil intent.
- Blind versus through, thread depth, unused depth, interruptions, thin walls.
- Machine sync / rigid tapping notes, holder type, and stick-out method if known.
- Acceptance gauges or inspection method; first-off notes.
- Identifiers needed for repeat orders.
Browse live constructions here: taps and carbide drill bits. When a thread mill may be the better path, browse thread mills. Open the request form when the package is ready: custom cutting tool RFQ.
Confirm the specification with engineering support
Before production ramp, confirm the 1/4 callout with TPI, cut versus form, prep-hole size with units, percent-of-thread or class intent, material condition, hole type and depth, and acceptance method with engineering. Hand the package to a product and RFQ path for a matched tap and drill recommendation, not a catalogue guess. HENTRY / HC supports drawing-based tap and carbide drill proposals. No price, MOQ, or unverified lead time is stated on this page.
Specification fields to confirm
- Proposed tap model or drawing (cut or form) and matching drill designation (#7, #3, or maker form size).
- Thread callout: 1/4-20 UNC or 1/4-28 UNF, class if known.
- Percent-of-thread or engagement target and check method.
- Material grade / condition and lubricant mode.
- Blind / through, depth, unused clearance, interruptions.
- Machine sync / holder / stick-out notes if known.
- Inspection and sample acceptance expectations.
- Identifiers needed for repeat orders.
Trial plan (minimum)
- Same drawing revision and acceptance criteria as the checklist.
- First-off record of torque feel, chip or form signal, gauge result, and hole size before compensation edits.
- Change one variable at a time when comparing #7 versus #3, percent of thread, or cut versus form under the same material and acceptance intent.
- Stop when torque grows abnormally, crests look incomplete, gauges fail, or the tap breaks.
- Do not claim a drill size "won" without those controls.
Review listed constructions here: explore taps · explore carbide drill bits · explore thread mills. Research and practice portals such as this CIRP research portal (also cited above) and tooling resource literacy such as this tooling resources overview support industry literacy only.
Request a 1/4 tap drill / tap recommendation
Suggested enquiry subject: 1/4 tap drill - [1/4-20 or 1/4-28] - [cut/form] - [material] - [blind/through] - [drill size]
1/4-20 Tap Drill Size FAQ
What size drill bit for a 1/4-20 tap?
For a cut tap on 1/4-20 UNC, published shop charts commonly list a #7 drill (0.2010 inch) at about 75 percent of full thread. Confirm the print class, material, and whether the method is cut or form. A form tap needs a larger prep hole from the tap maker chart. This answer is chart consensus, not an HC measured life or strength percentage.
What size drill bit for a 1/4-28 tap?
For a cut tap on 1/4-28 UNF, many public charts list a #3 drill (0.2130 inch) near the 75 percent basis. Do not reuse the #7 from the 1/4-20 row. Form taps still need the maker form-drill window, which is larger than the cut-tap row.
Why is the 1/4-28 cut-tap drill larger than the 1/4-20 drill?
Both share a 0.250 inch major diameter, but 28 TPI is a finer pitch than 20 TPI. At a comparable engagement target, less material must be removed, so published cut-tap charts step from about #7 (0.2010 inch) up to about #3 (0.2130 inch). Always lock TPI on the traveler before picking a letter drill.
Can I use the same drill for a form tap on 1/4-20?
No. Form taps displace material into the thread form, so the prep hole must be larger than the cut-tap #7. Reusing the cut-tap drill often causes swell, incomplete crests, or excess torque. Choose method first, then use the tap maker form-drill chart. This page does not invent a universal form letter matrix.
Is a bolt clearance hole the same as a 1/4-20 tap drill?
No. A tap drill leaves material so the tap can cut or form the internal thread. A bolt clearance hole is intentionally larger so the bolt shank passes without engaging threads in that plate. Do not treat clearance sizes as tap drills. A dedicated clearance-hole chart will cover fit classes after it publishes.
What does about 75 percent of thread mean on these charts?
Many commercial cut-tap charts aim near 75 percent of full thread as a shop convention for general mechanical work. It is a chart basis, not a guarantee of strength for every grade, and not an HC laboratory result. Hard materials or deep blind holes often push shops toward a lower percent to protect the tap. Confirm class and acceptance method on the print.
Which inputs should I send in an RFQ for 1/4 tap drill selection?
Send drawing revision, 1/4-20 or 1/4-28 callout, cut versus form or open, percent-of-thread or class intent, proposed drill size with units, material and lubricant intent, blind versus through and depth notes, acceptance method, and trial notes. Leave unverified life and price fields blank.
When does this page not apply?
It does not apply when you need invented life percentages, prices, ROI, or unverified case counts; when you need an unconditional best-drill ranking; when you need a full metric/UNC/UNF encyclopedia instead of the 1/4 20/28 OWN; when you need a dedicated 5/16, 10-32, or clearance-hole book; when you need a pasted universal form-tap size matrix; or when TPI, method, and acceptance notes are missing. Fix the inputs first.
Sources and related guides
Outbound references support Unified inch thread naming, public UNC/UNF tap-drill chart literacy, tapping and threading education, metrology and units portals, toolholding and cutting-data literacy, and manufacturing research portals cited in the body. Manufacturer-specific tap drill charts remain tied to their own products. The decision walkthrough is an HC editorial teaching aid, not a measured customer result. Sources checked 24 October 2026 (Asia/Shanghai).
- Codes and standards portal (public standards entry; linked in body)
- Laboratory UNC/UNF screw table (public lab table; linked in body)
- UNC UNF and metric tap drill chart (third-party reference; linked in body)
- Tap drill reference table (third-party reference; linked in body)
- Tap drill chart sizes overview (third-party education; linked in body)
- CNC threading and tapping overview (third-party education; linked in body)
- Tap drill sizes help page (third-party distributor education; linked in body)
- Threading knowledge overview (third-party education; linked in body)
- Tapping knowledge overview (third-party education; linked in body)
- Public metrology laboratory entry (public metrology entry; linked in body)
- Weights and measures overview (public metrology entry; linked in body)
- NIST SP 811 units guidance (public metrology entry; linked in body)
- NIST SP 811 publication PDF (public metrology entry; linked in body)
- National standards overview (public standards entry; linked in body)
- Engineering calculators portal (third-party tooling education; linked in body)
- Tool holder technology overview (third-party education; linked in body)
- Cutting data notes portal (third-party tooling education; linked in body)
- CIRP research portal (third-party research society; linked in body)
- Bolt science portal (third-party fastener mechanics literacy; linked in body)
- Tooling resources overview (third-party tooling literacy; linked in body)
Related live guides: tap drill size chart · form tap vs cut tap · thread milling vs tapping aluminum · precision holemaking selection guide · taps · carbide drill bits · thread mills · Knowledge hub · custom cutting tool RFQ. Dedicated 5/16 and 10-32 tap-drill pages and a bolt clearance-hole chart will be linked after they publish (soft-note until live).