
Early breakage and inconsistent tool life can have several causes. Identify the first abnormal event, then check the assembled setup, tool condition, chip evacuation, coolant delivery, and drilling cycle before assigning a cause. Also verify that the exact drill is approved for the required depth, material, and coolant arrangement, not only that flute length looks long enough. Change one variable at a time when isolating a mechanism, and stop the test if load, sound, chip return, coolant delivery, or edge condition changes abruptly.
OWN (this page): stage-based diagnosis of early solid-carbide-drill breakage and inconsistent tool life, plus a controlled-trial / failure-record method.
Sibling OWN: six shop checks before reorder. Keep that checklist page; do not merge. See solid carbide drill breakage causes.
Use this sequence before you change feed, swap brands, or scrap a lot of parts:
- Name the failure stage: entry, steady cut, peck or re-entry, breakthrough, retract, or life-curve shift.
- Preserve the drill, chips, and drawing; photograph edges before cleaning.
- Measure assembled runout and projection with a stated method and position.
- Review chips and coolant delivery together, not as separate stories.
- Map the exact cycle, including spot, peck, dwell, breakthrough, and retract.
- Confirm material condition and the drill application range for depth and coolant.
- Run a one-variable controlled trial with stop and acceptance criteria.
Diagnose · Mechanisms · Field signals · Symptom table · Checklist · Trial record · Failure review · FAQ
Diagnose the Failure Stage Before Changing the Process
A broken drill shows the final event. It does not identify the first event. The useful question is where the process first becomes abnormal: at entry, during steady cutting, during a peck or re-entry, at breakthrough, during retract, or only after a repeatable number of holes.
This distinction changes the next check. An entry failure directs attention to alignment, surface condition, drill projection, and point engagement. A failure deep in the hole makes chip transport and coolant delivery more important. Damage at breakthrough points toward uneven edge loading, exit geometry, or loss of support. A life curve that changes from batch to batch requires comparison of setup, material condition, coolant condition, and the tool lot before a new cutting parameter is accepted.
Use this seven-step decision process
- Stop and preserve the evidence. Record the failed hole number, cycle stage, machine message, spindle load trend, sound change, and whether the drill broke in the part. Keep the drill, chips, and affected component for inspection.
- Inspect before cleaning. Photograph the drill point, corners, margins, and flutes. Note built-up material, polished lands, chipped corners, asymmetric wear, heat tint, and packed chips. Balanced wear is the target; uneven wear is evidence that the process needs investigation.
- Measure the assembled system. Check runout at a defined position on the assembled drill, holder, and spindle interface; inspect the collet or chuck, contact surfaces, tool projection, spindle condition, and workholding. For small or slender drills, use a method that does not deflect or damage the tool. State the measuring position and method; a shank reading does not establish cutting-edge runout. Manufacturer drilling guidance treats low runout as essential to process security, tool life, and hole quality.
- Review chips and coolant together. Compare chip form at entry, steady cutting, and exit. Confirm that coolant reaches the cutting zone and that pressure, flow, concentration, filtration, and temperature are recorded rather than assumed. Chip formation depends on the workpiece, drill geometry, coolant pressure and flow, and cutting data.
- Map the exact cycle. Record spot or pilot operation, drilling depth, peck depth, full or partial retract, dwell, re-entry, breakthrough, and retract feed. Record whether re-entry encounters retained chips, rubbing, or a previously worked surface. For materials susceptible to work hardening, assess whether the actual cycle may be contributing to that condition.
- Check the workpiece and tool specification. Confirm material grade, condition, hardness or heat treatment, casting or surface condition, entry and exit geometry, hole depth-to-diameter ratio, drill revision, coating, coolant-hole design, and regrind status.
- Run a controlled trial. Keep the baseline tool and one comparison condition. Change one variable, define the sample size, inspect at planned intervals, and use the same stop and acceptance criteria. A lower breakage count is not enough if hole quality, cycle time, or wear predictability becomes worse.
Do not continue a production trial after a sudden load increase, intermittent drilling sound, loss of chip return, coolant interruption, visible corner damage, or a shift in hole quality. These observations may precede tool breakage or component damage.
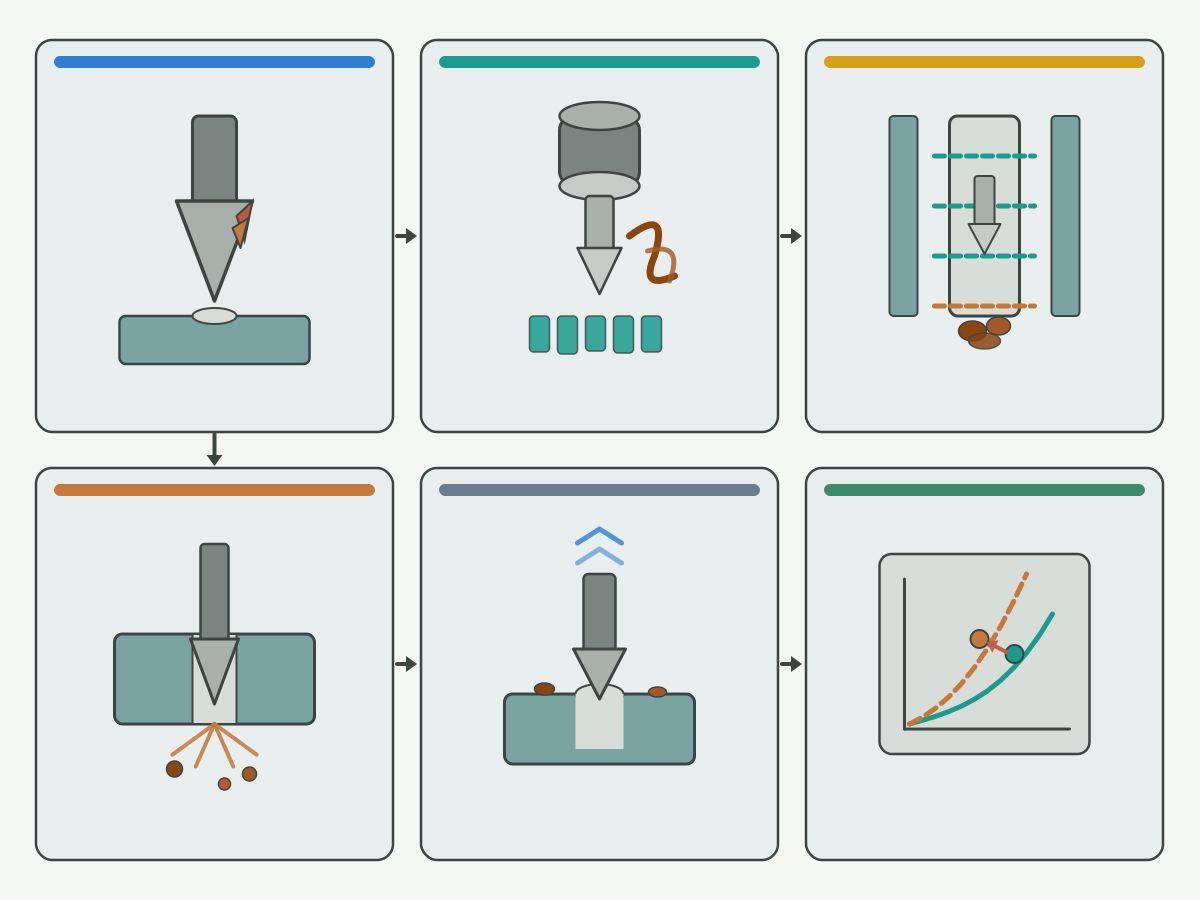
Illustration (not a photo). Collect evidence where the first abnormal event appears; the fracture location alone does not identify the initiating event. Stages named only in caption and surrounding body (no text on the image): entry → steady cut → peck / re-entry → breakthrough → retract → life-curve shift.
Related diagnostic task: Six shop checks before reorder. Solid carbide drill breakage causes.
Why Early Breakage and Inconsistent Life Occur
Runout, alignment, and tool projection
A symmetrical solid carbide drill should load both cutting edges as evenly as the application allows. Runout, spindle-to-axis misalignment, worn or contaminated holder interfaces, excess projection, and weak workholding can place more load on one edge. The resulting pattern may appear as one-sided margin wear, uneven corner chipping, oversized holes, or short and scattered life.
Measure the assembled condition instead of relying only on holder type or a machine specification. Remove and clean the components, inspect contact surfaces, use the shortest practical projection, and compare wear on both cutting edges. For a small or slender drill, define a measuring position and method that do not bend the tool. A shank reading can help assess the clamping system, but it does not by itself prove cutting-edge runout.
Published manufacturer guidance for rotating drilling states that tool runout should not exceed 0.02 mm (0.0008 in / 20 µm) when close hole tolerance, surface finish, and consistent tool life are required. That value is application guidance for the sources that publish it, not a universal acceptance limit for every drill and spindle. One manufacturer application note for heat-resistant alloys also states solid-carbide drill runout must not exceed 0.001 in TIR under the conditions of that note. Validate the acceptance limit for the actual drill, holder, and spindle. For drills used axially in a lathe, also check the relationship between the rotary axis and the drill axis; axis alignment error, unstable workholding, and entry wander are documented breakage mechanisms in manufacturer troubleshooting handbooks.
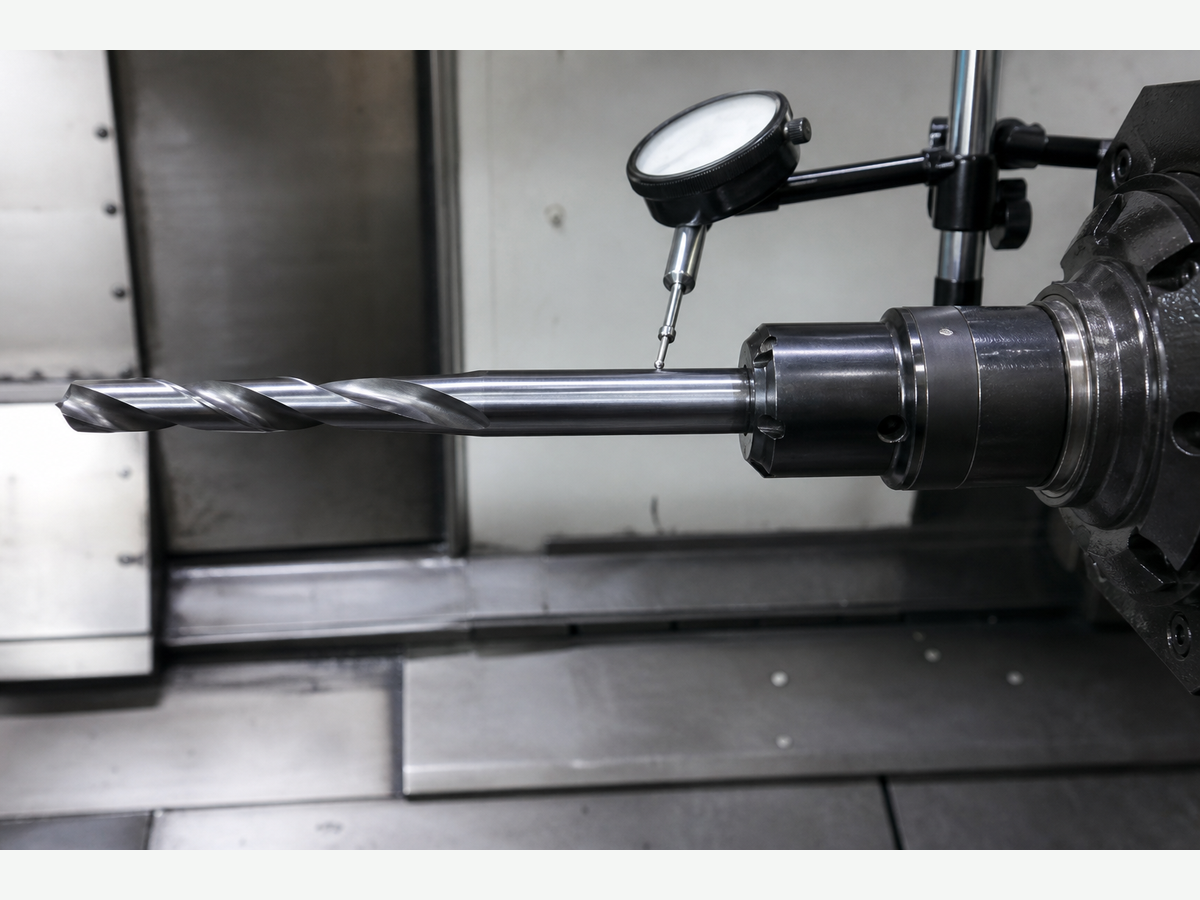
See also this manufacturer drilling knowledge overview on tool run-out and this tips film on minimizing tool run-out in rotating applications.
Chip formation and evacuation
The flute is both a cutting geometry and a transport path. If chips become long, compressed, welded together, or scratched by recutting, torque and radial loading can rise before the drill breaks. The problem may originate in cutting data, drill geometry, material behavior, coolant delivery, or a combination of them.
Do not judge the process from chips found in the machine after the shift. Collect chips from a known hole and stage. Compare entry chips, steady-state chips, and breakthrough chips. Manufacturer drilling guidance treats suitable chip form and evacuation as central to process security, tool life, and hole quality, and notes that poor chip evacuation can move the drill radially. Scratch marks on chips are a published sign of chip jamming. Peripheral "needles" on the entrance chip are linked to imbalance from runout, inclined entry, excessive feed, unstable conditions, or corner damage.
For a named multi-material solid-carbide drill family, published how-to guidance notes that when chip jamming causes fluctuating torque, increasing feed per revolution by 10-20% while holding cutting speed can help stabilize the cut, only within that product's recommended window, and only after delivery and chip form have been inspected. Chip-form literacy: this tips film on analyzing chip formation.
Related HENTRY pages: carbide drill chip packing checklist · carbide drill speeds and feeds.
Coolant route, flow, and filtration
A pressure reading at the pump does not prove that useful coolant reaches the drill point. A partially blocked channel, leakage at an interface, inadequate flow for the flute volume, poor nozzle aim, unstable concentration, or contaminated coolant can leave the cutting edge hot and the chip path congested.
Record pressure and flow where the system permits, inspect filters and coolant holes, confirm the actual route through the holder, and observe chip return. Treat manufacturer pressure or flow guidance as tool-specific.
Condition-bound examples from published manufacturer pages (not universal shop limits):
| Published guidance (condition-bound) | Applicability boundary |
|---|---|
| Internal coolant necessary for hole depths > 3×DC to help avoid chip jamming | Named solid-carbide drill how-to / general drilling tips from the same manufacturer family |
| Minimum recommended coolant pressure 10 bar (145 psi) | Same product how-to; not a transfer value for every diameter or series |
| Micro-drilling typical coolant pressure 40-70 bar | Manufacturer micro-hole drilling guidance |
| About 40 bar recommended for chip evacuation in deeper holes > 20×D | Named deep-hole product how-to |
| High-pressure coolant around ~70 bar discussed for chip security and life benefits | Manufacturer drilling tips (system and filtration dependent) |
| Emulsion oil content 5-12% (often 10-15% for stainless and heat-resistant alloys) | Manufacturer coolant tips; confirm with fluid supplier |
| Coolant tank volume 5-10× the pump delivery per minute | Manufacturer coolant tips |
| Horizontal internal stream without downward drop for at least 30 cm | Manufacturer quick check for flow at the tool |
| External coolant: at least one nozzle aimed near the tool axis (two if the drill is stationary) | Manufacturer external-coolant tip |
| Dry drilling only for short-chipping materials up to about 3×D; not recommended for stainless (ISO M) or heat-resistant (ISO S) materials | Manufacturer dry-drilling tips |
| Coolant pressure/flow reference curves differ for L/D = 5 vs L/D = 30 across diameter classes | Manufacturer solid-carbide coolant reference diagrams (lab conditions; field deviations expected) |
A published coolant-fed micro-drill procedure for a named 8×D series versus a named 15×D series uses different preparation methods. That guidance must not be transferred unchanged to another drill geometry or diameter. Primary pages: this manufacturer drilling tips page on coolant and chip control, this solid-carbide coolant pressure and flow reference diagram (PDF), and related HENTRY guidance on when through-coolant is required.
Entry, breakthrough, and interrupted engagement
A sloped, curved, rough, or interrupted surface does not load both cutting edges at the same time. That uneven engagement can deflect a small drill, promote vibration, and chip an edge. Cross holes and pre-drilled features can create a similar interruption. Manufacturer irregular-surface guidance states that irregular surfaces can cause excessive uneven forces and that small-diameter drills may deflect, wander, or break. It also warns that pre-drilled holes can chip a solid carbide drill under the conditions described.
Condition-bound feed and geometry examples from that irregular-surface guidance for solid carbide drills (validate against the exact tool family):
- Irregular surfaces: reduce feed to 25% of the recommended rate until the full diameter is in cut.
- Inclined entry: keep the tip entering first; published maximum recommended angle from center to corner is 6°; reduce feed to 1/3 of normal during entrance when following that page.
- Convex surfaces: radius greater than 4×DC; feed 50-100% of recommended until full diameter is in cut.
- Concave surfaces: radius greater than 15×DC; reduce feed to 30% of recommended until full diameter is in cut.
- Crossing an existing hole (depths below 12×D on that page): reduce feed to 25% of recommended during entrance and exit of the crossing.
- Inclined exit (solid carbide section on that page): published maximum recommended exit angle 30°, with feed reduced to 1/3 of normal during exit.
- Exit / burr control on a named product how-to: slow exit feed to about 30% of recommended; reduce feed by 50% just before breakthrough for burr control.
Verify entry and exit geometry from the drawing and the actual component. If the application requires a spot, pilot, or milled flat, the geometry of that preparation must match the drill manufacturer's method. A pilot that is too large or has an incompatible point may load the drill at the corners instead of guiding it. Source page: this manufacturer irregular-surface drilling guide.
Pecking, re-entry, and cycle design
Pecking is not automatically protective. A cycle may improve chip clearance in one process and create repeated impact, rubbing, chip recutting, or coolant interruption in another. Long dwell periods can also change the thermal and surface condition at the bottom of the hole.
Document each motion. Review whether the drill fully exits the hole, how it re-enters, whether chips remain in the flute, and whether coolant is interrupted. Compare the cycle with the drill supplier's procedure for that diameter, depth, and coolant design.
Related HENTRY pages:
- When peck drilling is required
- When through-coolant is required
- Deep-hole L/D, peck, and chip escape
- Carbide drill speeds and feeds (process-first)
One multi-material solid-carbide assortment publishes micro drills up to about 6×D and deep-hole drills from 12×D to 30×D (product-range figures, not a shop depth approval by themselves). For drills with a published length of 15×D or greater, the same manufacturer how-to recommends a pilot using a short-hole drill of 3-5×D (minimum 1.5×D) at the same diameter. A published 15×D micro-precision procedure from another manufacturer recommends a compatible pilot of at least 1×D, entering the pilot at a maximum of 300 rpm and 20 ipm, starting high-pressure coolant before ramping to operating speed, drilling to depth without pecking, and slowing to a maximum of 300 rpm before retract, only for that named series and dimensions. The same family publishes an 8×D internal-coolant series with a 135° point; the 15×D procedure pairs a 140° pilot series and defines usable flute depth with t_max = l2 - 1.5 × d1. Web thinning is stated from about Ø 1.40 mm upward on those sheets. None of these values is a universal microdrilling recipe. Supporting product how-to: this named multi-material solid-carbide drill how-to / application page, this named 8×D micro-precision series sheet (PDF), and this named 15×D micro-precision procedure extract (PDF).
Material condition and tool application match
The same material name can hide changes in hardness, heat treatment, scale, inclusions, casting condition, or batch. Stainless steel, alloy steel, and cast aluminum also create different heat, adhesion, chip, and wear behavior. A drill that worked in one condition may not behave the same after the material state, entry surface, or hole depth changes.
Confirm the exact material and condition before comparing brands or grades. Then verify the drill's application range, point geometry, coating, margin design, flute capacity, and coolant configuration. If the change cannot be isolated, treat the cause as unresolved and run a bounded trial rather than declaring a tool defect or parameter error.
Related product decision: Solid carbide drill product family.
Wear limit and planned change criterion
A drill can appear acceptable until accumulated wear raises force or disrupts chip formation. If the tool is run to random breakage, the process converts gradual wear into unpredictable scrap risk. The change criterion should be tied to an observable condition such as a documented wear pattern, hole quality trend, spindle-load behavior, or accepted-hole count under a controlled process.
Inspect new, mid-life, and end-of-life tools at fixed intervals. Manufacturer wear guidance recommends balanced wear and links uneven wear with shorter life, breakage, and component damage. Excessive wear is a published precursor to overload and breakage. Where built-up edge cannot be fully avoided, one wear guide suggests calculating a speed that places BUE in the strongest part of the drill (about 50% of diameter), as diagnostic guidance, not a production default. Wear literacy: this manufacturer drilling wear and troubleshooting page and this tips film on analyzing tool wear in solid carbide drilling.
Three Field Signals That Show Why a Stage-Based Method Matters
The following examples are public shop-floor discussions, not controlled HENTRY case studies and not verified life conclusions. They demonstrate recurring decision problems. The reported numbers and observations belong only to the cited threads, and the proposed causes in replies remain hypotheses until measured in the actual setup.
Field signal one: 304 stainless production backlog
A Practical Machinist discussion described a 6.35 mm diameter by 12.7 mm deep hole in 304 stainless steel, a production requirement of about 11,000 holes, and catastrophic failures that included broken corners and microchipping. The post also reported through-tool coolant and a growing machine backlog.
The useful response is not to select a new feed from the thread. It is to separate the failure stages, inspect the earliest edge damage, verify assembled runout and coolant delivery, and compare one controlled change against a defined stop condition. That process can distinguish progressive wear from an entry, chip, or delivery problem. Thread (field signal only): Carbide Drill Trouble.
Field signal two: wide life variation in annealed 4140
Another discussion reported 3 mm solid carbide drilling about 15.1 mm deep in annealed 4140 steel. The poster described some drills lasting only 50 to 200 parts while others reached roughly 2,000 to 2,500 parts. Each part contained four holes. Broken drills could scrap components. The setup used an axial live tool, external water-soluble coolant, and a peck cycle.
The poster also reported using a nominal 3×D drill for a hole approximately 5×D deep, based on available flute length. Before interpreting the life variation as a supplier or setup issue, verify the permitted drilling depth and chip-evacuation conditions for that exact tool. Available flute length alone does not establish application suitability. The reported life spread remains a signal to investigate, not proof of a tool-lot or process cause.
The next step is a lot-by-lot record of drill source, approved application depth, assembled runout, holder and spindle condition, material batch, coolant state, cycle, wear at fixed intervals, and failure stage. Thread (field signal only): Solid Carbide Drills Breaking Looking for Recommendation.
Field signal three: microdrill breakage near ten times diameter
A third discussion described a 0.79 mm drill making holes through 7.94 mm MIC-6 cast aluminum plate, close to a 10× diameter application. Each plate required about 800 holes. The poster reported 10,000 rpm and a 0.030 in peck depth, with feed changed from 9 in/min to 6 in/min. An earlier process was reported to reach about 2,000 holes at the higher feed; subsequent drills were reported to break around 1,000 holes after the feed reduction.
These are historical, self-reported conditions, not recommended settings. The observations do not isolate feed as the cause of the later breakage. The two life figures do not represent a controlled same-condition comparison. A break could also scrap a large mold plate depending on its location.
At this scale, small changes in runout, point entry, projection, chip packing, and coolant access can consume a large share of the available process margin. A published coolant-fed microdrilling procedure may require a compatible spot or pilot operation and internal coolant; it must be matched to the actual drill series rather than copied as a generic recipe. Thread (field signal only): Any Advice for 1/32 Carbide Drill at 10x Depth.
Match the Symptom to the Next Controlled Check
Use the table to choose the next evidence to collect. It ranks checks by observable pattern; it does not declare a root cause without measurement.
| Observed pattern | First evidence to collect | Next controlled check | Do not assume |
|---|---|---|---|
| Breaks at entry | Entry surface, point damage, runout, projection, alignment | Shorter projection or verified preparation method with all other variables fixed | That speed alone caused the failure |
| Chips or breaks deep in the hole | Chip form by depth, flute packing, coolant route and return | Confirm delivery and compare one cycle or coolant change | That pump pressure equals point delivery |
| Corner chips at breakthrough | Exit geometry, burr change, edge symmetry, retract event | Controlled exit strategy within supplier guidance | That the drill grade is too brittle |
| One edge wears faster | Assembled runout, holder contact, spindle and workholding | Clean, reassemble, measure and repeat with the same drill lot | That a new holder name guarantees alignment |
| Life varies widely by tool or batch | Tool lot, material batch, coolant condition, setup changes and wear intervals | Blocked comparison with one recorded variable changed | That brand is the only variable |
| Breakage begins after a repeatable hole count | Wear trend, hole quality, load, chips and edge photos before failure | Set a planned change point below the verified failure zone | That running to fracture gives maximum value |
Procurement and Validation Checklist
A replacement drill cannot be compared fairly without a shared application record. Mark unknown fields as unknown and resolve them during technical review rather than filling them with estimates.
- Workpiece and feature: Material grade and condition, hardness when relevant, casting or surface condition, hole diameter, depth, blind or through hole, entry and exit geometry, cross holes, interrupted surfaces, tolerance and surface requirement.
- Machine and setup: Machine model, spindle interface, rotating or stationary drill, holder and collet, tool projection, measured assembled runout, workholding method and axis alignment where relevant.
- Coolant and chips: Internal or external supply, coolant type and concentration, recorded pressure and flow where available, filtration, nozzle position, channel condition, chip form and how chips were collected.
- Cycle and parameters: Spindle speed, cutting speed, feed per revolution, feed rate, spot or pilot operation, peck distances, dwell, breakthrough, retract and any adaptive or load-monitoring behavior.
- Current tool: Manufacturer, product code, diameter, length-to-diameter ratio, geometry, coating, coolant-hole design, shank, lot, regrind history and the supplier's application guidance.
- Failure evidence: Hole number, failure stage, spindle load or alarm, sound change, chips, edge and flute photographs, broken fragment location, hole inspection and whether the part was accepted or scrapped.
- Trial acceptance: Planned sample, inspection frequency, wear limit, hole quality criteria, accepted-hole or accepted-part measure, cycle-time limit, stop condition and decision rule for retain, adjust, trial or replace.
Drill Failure and Controlled-Trial Record
Complete one record for the baseline and one for each trial condition. Use hole count and part count as separate fields, and identify every photograph or machine record so the conclusion can be traced back to evidence.
| Field group | Required record | Entry or evidence reference |
|---|---|---|
| Baseline conditions | Material batch and condition; hole diameter and depth; drill reference, revision and lot; permitted application depth | Record or attach |
| Assembly | Holder and collet; projection; spindle interface; measuring position; runout method and result | Record or attach |
| Cycle | Spot or pilot operation; peck distances; dwell; re-entry; breakthrough; retract; cutting data | Program revision or record |
| Coolant and chips | Route; type and concentration; pressure and flow where available; filtration; chip samples by stage | Record or photo ID |
| Failure evidence | First abnormal stage; hole and part count; load or alarm; sound; edge, flute and component observations | Photo or machine record ID |
| Controlled change | The one variable changed for an isolation test; conditions intentionally retained; reason for the change | Trial revision |
| Acceptance | Hole quality; wear criterion; accepted holes or parts; cycle-time limit; inspection interval; stop rule | Measured result |
| Conclusion | Hypothesis supported; hypothesis not supported; or evidence insufficient; next action | Decision and owner |
Keep the Acceptance row intact in one table. Do not split a single acceptance item across page breaks in layout.
How HENTRY Can Support the Next Validation Stage
HENTRY can use the application record to support technical preselection and a controlled comparison plan for a solid carbide drill. The first review should identify missing conditions, the likely failure stage, and the evidence needed before a tool or geometry change is proposed. A quotation should follow the engineering task, not replace it.
For a useful first review, include the material and condition, hole drawing or dimensions, machine and holder, coolant route, current drill specification, cycle description, failure stage, chip photographs, edge-wear photographs, and production target. Unknown values can be marked for follow-up.
Next action: Prepare one baseline record and one controlled-trial record. Use the checklist above so the comparison measures accepted holes and wear progression under documented conditions.
Request a Drill Failure Review
Describe the material, hole dimensions, current drill, and failure stage in the message. Contact HENTRY to arrange transfer of drawings and photographs. Use the English contact / RFQ page: Request a Drill Failure Review.
The public contact page states that a drawing can be attached when available and that drawings are stored privately for the engineering team. Do not assume a specific attachment widget is visible in every browser session; if upload is unavailable, email the drawing and photos to the address shown on the contact page after describing the failure stage in the form message.
Product path for series selection after diagnosis: Solid carbide drills.
Frequently Asked Questions
Should speed or feed be reduced first?
Not without identifying the failure stage and wear pattern. Lower values may reduce one load while worsening rubbing, heat, or chip form in another process. Check the drill supplier's application guidance, then change one parameter after runout, stability, chip evacuation, and coolant delivery have been reviewed.
Does through-coolant prevent drill breakage?
No. Through-coolant can improve access to the cutting zone, but useful delivery still depends on flow, pressure, channel size, filtration, interfaces, and chip path. A system can show pressure while a channel is restricted or the available flow is inadequate for the application.
Is peck drilling safer for a deep hole?
Only when the drill and application require it. Pecking can assist chip management, but repeated retract and re-entry can also recut chips, interrupt coolant, or shock the cutting edge. Follow the procedure for the exact drill series, diameter, depth, and coolant design.
When should a drill be replaced before it breaks?
Set the change point from a controlled life study. Inspect tools at planned intervals and relate wear, load, chips, and hole quality to accepted production. Replace the drill before the verified process enters the zone where edge damage or output variation rises.
How should two drill suppliers be compared?
Compare the same workpiece task, quality requirements, and cost basis. Use approved operating conditions for each drill and record any differences in holder, coolant, pilot strategy, cycle, and cutting data. If several conditions change, describe the result as a comparison of complete process solutions. Use a one-variable test only when the purpose is to isolate a specific mechanism.
What does stage-based diagnosis mean for a broken drill?
It means naming where the process first became abnormal (entry, steady cut, peck or re-entry, breakthrough, retract, or life-curve shift) before changing parameters or tooling. The fracture location alone does not identify the initiating event. Preserve the drill and drawing, then collect stage-matched evidence.
Can flute length alone prove a drill is approved for hole depth?
No. Available flute length does not establish permitted drilling depth, chip-evacuation capability, coolant design, or application approval. Confirm the manufacturer's depth rating and procedure for that exact series, diameter, and coolant arrangement before interpreting short or scattered life.
What should you send for a drill failure review?
Send material and condition, hole dimensions or drawing, machine and holder, coolant route, current drill specification and lot, cycle description, named failure stage, chip and edge photographs, and the production target. Mark unknowns instead of inventing numbers. Do not include price targets or invented life percentages.
Sources and Related Content
Manufacturer guidance below supports the general diagnostic method. Product-specific limits remain applicable only to the stated tool and conditions. The three forum discussions are field signals and do not establish verified root causes. Authoritative quantitative proportion for this revision is recorded in the evidence audit (44 / 62 ≈ 71% under listed itemization; forums not in the numerator).
Authoritative manufacturer / primary technical sources
- Drilling a hole: tool run-out (≤ 20 µm) - Sandvik Coromant. Supports: runout limit guidance for successful hole drilling. Boundary: published general drilling knowledge; validate on the actual spindle and drill.
- Drilling tips: coolant, chip control, dry drilling - Sandvik Coromant. Supports: emulsion ranges, tank volume, internal coolant preference above 3×DC, horizontal stream check, HPC ~70 bar discussion, dry-drilling limits. Boundary: general tips; confirm fluid chemistry with the coolant supplier.
- CoroDrill Dura 462: how to use / product application - Sandvik Coromant. Supports: runout ≤ 0.02 mm; internal coolant > 3×DC; min 10 bar; pilot 3-5×D for ≥15×D; exit ~30%; breakthrough feed -50%; ~40 bar for >20×D; fn +10-20% for chip-jam torque. Boundary: named product family only.
- Irregular surface drilling - Sandvik Coromant. Supports: feed reductions and geometry limits for irregular, convex, concave, inclined, and cross-hole conditions; small-diameter deflection/breakage risk. Boundary: values vary by drill type section on the page; do not mix insert-drill and solid-carbide rows.
- Drilling wear and troubleshooting - Sandvik Coromant. Supports: balanced flank wear target; breakage causes including runout, chip jamming, and insufficient coolant; BUE location guidance (~50% of diameter). Boundary: diagnostic tables; corrective data must be revalidated.
- Tips film: How to minimize tool run-out in rotating applications - Sandvik Coromant. Supports: clean interfaces, short projection, runout importance. Boundary: tips film; numerical limits must be taken from the paired knowledge pages.
- Tips film: Analyze tool wear in solid carbide drilling - Sandvik Coromant. Supports: inspect wear before breakage; uneven wear as a process signal. Boundary: tips film paired with the wear troubleshooting page.
- Tips film: How to analyze chip formation - Sandvik Coromant. Supports: chip form depends on material, geometry, coolant pressure/flow, and cutting data. Boundary: visual examples require application-specific interpretation.
- ExclusiveLine micro-precision drills: 8×D series sheet - Guhring. Supports: published 8×D cutting-depth series with internal coolant. Boundary: named series and dimensions only.
- ExclusiveLine micro-precision drills: 15×D procedure extract - Guhring series data via distributor datasheet. Supports: 15×D series; pilot ≥1×D; enter at max 300 rpm / 20 ipm; no pecking in that procedure; slow to max 300 rpm before retract. Boundary: named 15×D series only; do not merge with 8×D spot method into a generic recipe.
- Reference value diagrams for coolant pressure / flow: solid carbide drilling - Walter Tools. Supports: coolant pressure and quantity reference curves by diameter for L/D = 5 and L/D = 30. Boundary: laboratory reference values; machine, fluid, and pump cause field deviations.
- Kennametal material-subgroup application notes (solid carbide runout) - Kennametal via distributor PDF. Supports: solid-carbide drill runout must not exceed 0.001 in TIR in the heat-resistant alloy application note; hydraulic/precision chucks called out. Boundary: material-group note, not a global catalog limit for every grade. (HEAD from this box returned 403; keep as Sources anchor; fact retained from evidence audit.)
Field-signal citations (not counted toward authoritative quantitative numerator)
- Carbide Drill Trouble - Practical Machinist. Field signal: reported 304 stainless production breakage. Uncontrolled discussion.
- Solid Carbide Drills Breaking Looking for Recommendation - Practical Machinist. Field signal: reported life variation in annealed 4140. Uncontrolled discussion.
- Any Advice for 1/32 Carbide Drill at 10x Depth - Practical Machinist. Field signal: reported MIC-6 microdrill breakage including poster-stated 10,000 rpm and 0.030 in peck. Uncontrolled discussion.