
Product Detail
Gun Drills for Deep Hole Machining
Submit your hole dimensions, machine interface, and coolant setup to assess gun drill supply and application requirements.
Gun drills · deep hole tools
Gun Drills for Deep Hole Machining
Submit your hole dimensions, machine interface, and coolant setup to assess gun drill supply and application requirements.
- Send hole diameter, depth, and guidance method for review
- Match machine oil-feed interface and coolant capability
- Compare deep-hole carbide drill when that route fits better
Gun drill structure and supply object
This page sells gun drill tools — tip geometry, flute, driver/interface, and coolant path. It does not automatically expand into machining services or machine supply. Process boundaries and setup teaching stay on the gun drilling guide.
Single-flute / solid gun drill families
Confirm diameter, effective length, total length, and driver style from the print and machine. Unconfirmed series codes are not listed as stock.
Driver and oil-feed connection
Machine-side interface and oil-feed adapter must match. Photos of the current setup help when the interface code is unclear.
Deep-hole carbide drill route
Some duties fit a deep-hole solid carbide drill better. Open deep-hole carbide drills when L/D and coolant path point that way.
Hole diameter, depth, and guidance
Collect hole diameter, depth, entry condition, and guidance method (bushing / pilot / start hole). Do not publish a single “max L/D” for all gun drills — ratios are series- and setup-specific.
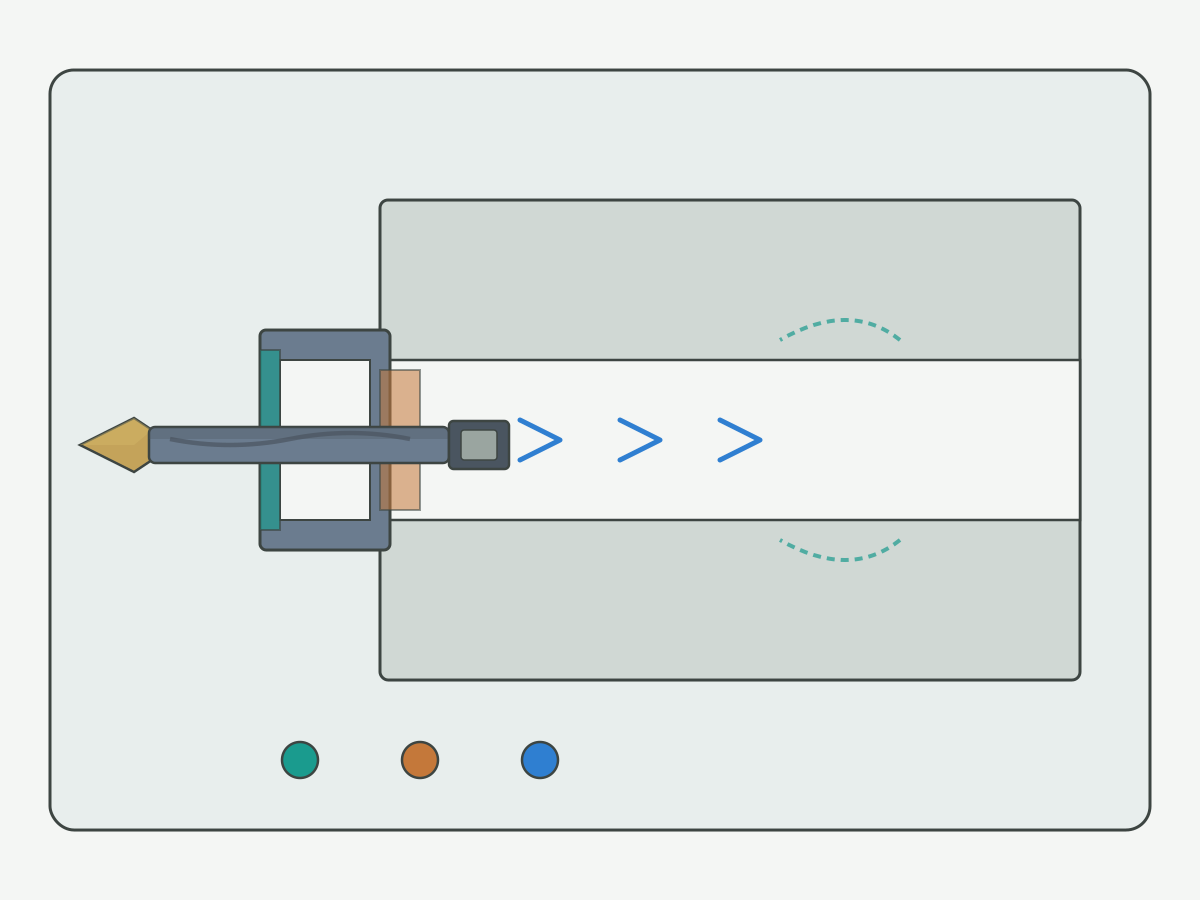
- Diameter & depth Finished hole size and depth from the print — not catalog marketing ranges.
- Entry / start Spot, pilot, or bushing start condition affects tip choice and walk.
- Guidance Bushing length, clearance, and alignment must match the process plan.
- L/D Treated as an engineering review input, not a universal published ceiling on this page.
Coolant interface and machine capability
Use a machine checklist: interface, coolant medium, pressure/flow capability, and filtration. Numeric values cite selected series data only — blank cells mean engineering confirm.
What to send
Machine model, spindle or oil-feed interface, coolant type, available pressure and flow, and filtration level.
If pressure or flow is unknown, say so — HENTRY will not invent a “standard” gun-drill pressure for every machine.
Workpiece material and chip evacuation
Material and chip requirements become a conditions table for engineering. Deep-hole process teaching stays on K009; this page keeps purchase-critical inputs only.
| Input | Why it matters | If unknown |
|---|---|---|
| Workpiece material / condition | Tip geometry and coolant strategy | Alloy + hardness band if known |
| Chip form / evacuation | Deep holes fail when chips pack | Describe prior tool behavior if any |
| Hole quality target | Size, straightness, finish expectations | State print tolerances · to your drawing |
Supply scope and quotation
Confirm HENTRY-available series, accessories, and any regrind service before quoting. Unconfirmed services are not written as promises. Compare with deep-hole carbide drills when that route fits better.
Selection guide
One row per duty. Empty numeric cells mean confirm from drawing / series data.
| Series / task | Structure | Diameter mm | Effective length mm | Total length mm | Interface | Guidance | Coolant |
|---|---|---|---|---|---|---|---|
| Gun drill review | Engineering confirm | to your drawing | to your drawing | to your drawing | Machine docs · confirm | Bushing / pilot · confirm | Pressure / flow · confirm |
| Deep-hole carbide alt. | See product page | to your drawing | to your drawing | to your drawing | Shank · confirm | Process-dependent | Through-coolant · confirm |
No universal max L/D is published here. Unconfirmed catalog rows are not shown as standard range.
Gun drills FAQ
Answers state decision conditions and next steps. They do not replace application approval.
Can a standard CNC machine use a gun drill?
Only if the machine can supply the coolant pressure, flow, filtration, and interface the selected gun drill requires — and if bushing or pilot guidance matches the process. Send machine model, coolant setup, and hole data for review. Do not assume a turret lathe or VMC is ready without that check.
What coolant information should I provide?
Coolant type (oil / emulsion), available pressure and flow, filtration level, and the spindle or oil-feed interface on the machine. Numeric limits come from the selected series data — blank cells here mean engineering confirm.
Does HENTRY provide deep-hole machining services?
This page is a tool supply page. Deep-hole process teaching stays on the gun drilling guide. Machining services are only stated after business-scope confirmation — they are not implied by tool sales.
When should I use a deep-hole carbide drill instead?
Compare duty, L/D, coolant path, and machine capability. See also deep-hole carbide drills. HENTRY will not force one family when the other fits the print better.
Request Gun Drill Selection
Page K008 · Product Gun Drills for Deep Hole Machining. Required: email, product or task, requirement description. Optional: drawing upload, company, material, sizes, machine, quantity. “Model uncertain” is allowed.
Footer / legal entity: Guangdong Hentry Tool Technology Co., Ltd Brand on page: HENTRY.